



Moldeo por inyección de plástico personalizado: Herramientas, Materiales, y Guía de Producción
Custom plastic injection molding works best for products that need repeatable quality, scalable production, and tight dimensional control. Success depends on choosing the right tooling, resin, and validation process before mass production begins. Buyers should evaluate mold type, Procedimientos de muestreo, production lead times, and supplier experience early to reduce revision costs, Retrasos, and long-term quality issues.
Custom molded parts can fail long before production starts if tooling, Materiales, or DFM decisions are rushed. A strong injection molding project is built around planning, not just machine capacity. Buyers need clear answers about tooling cost, resin selection, production timing, and validation steps before approving steel cutting or mass production.
What is custom plastic injection molding and when does it make sense?
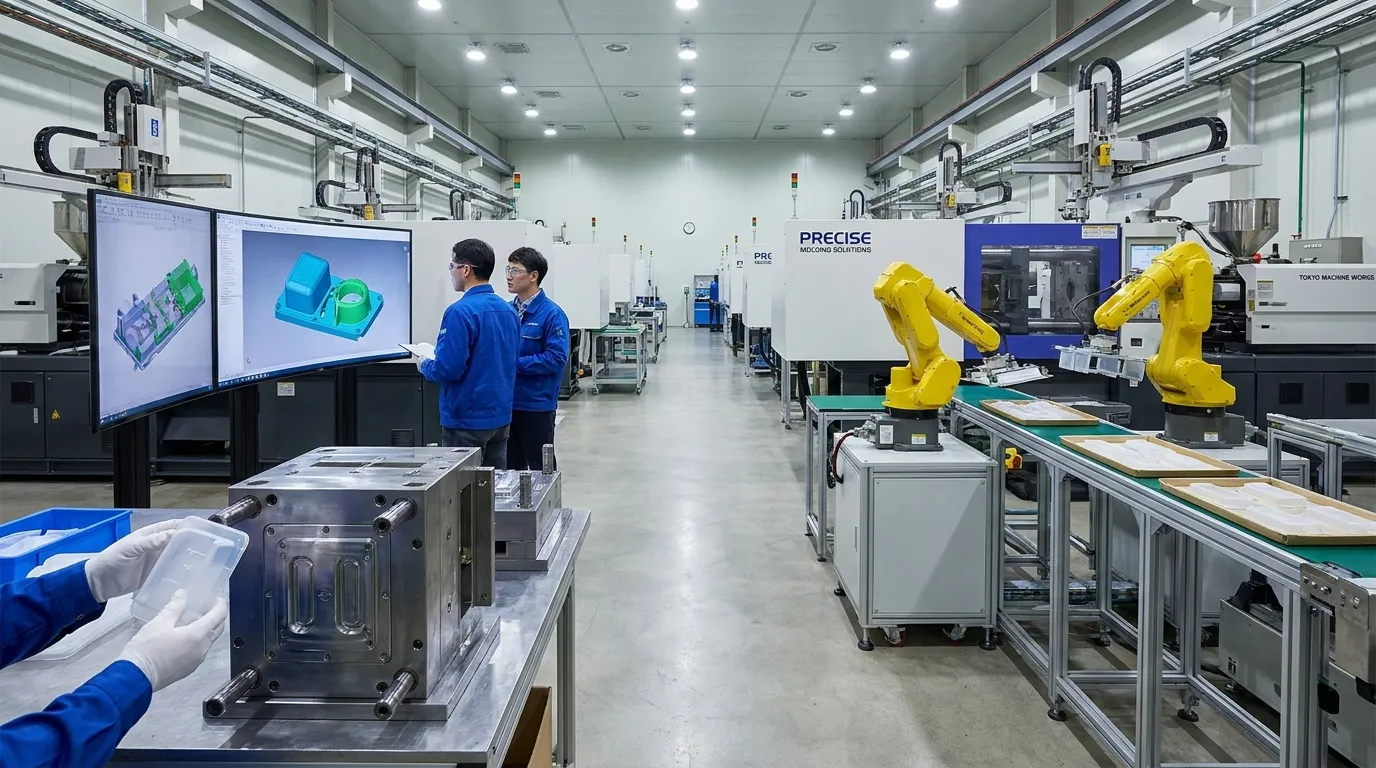
Custom plastic injection molding works best when a product needs repeatable quality, tight tolerances, and medium-to-high production volume. The process requires upfront tooling investment, but lowers per-part cost once production scales.
Injection molding creates plastic parts by injecting molten resin into a mold cavity under pressure. The same mold can produce thousands or millions of identical parts with consistent dimensions and surface finish.
The process makes sense when a product requires stable repeatability, cosmetic consistency, or complex geometry. Carcasas de electrónica de consumo, automotive clips, Componentes del electrodoméstico, and medical enclosures are common examples. Según Directorio IQS, injection molding remains one of the most widely used methods for large-scale plastic part production.
| Necesidad de fabricación | Ajuste por moldeo por inyección |
|---|---|
| Alto volumen de producción | Excelente |
| Tolerancias estrictas | Fuerte |
| Cambios rápidos en prototipos | Limitado después de la herramienta |
| Inversión inicial baja | Pobre |
| Acabado superficial cosmético | Fuerte |
| Salida repetible | Excelente |
Low-volume projects sometimes benefit from bridge tooling or aluminum molds. A startup producing 5,000 consumer electronics housings may use aluminum tooling first to reduce launch risk before moving to hardened steel tooling later.
For a broader overview of mold structures and tooling systems, véase el Guía de moldes de inyección.
How does the custom injection molding process work from design to production?
Most custom injection molding projects follow a predictable sequence: Análisis de DFM, tooling fabrication, Muestreo T1, Revisiones, Validación, and mass production. Problems become far more expensive once steel cutting begins.
A typical project starts with a DFM review, short for Design for Manufacturability. Engineers evaluate wall thickness, Ángulos de tiro, gating positions, material flow, and part geometry before tooling begins. Early DFM approval prevents expensive mold revisions later.
Once the design is approved, the manufacturer creates the mold tool. This stage includes CNC machining, EDM work, Pulido, fitting, and cooling channel preparation. The full Flujo de trabajo de producción de moldes usually takes several weeks depending on mold complexity.
Análisis de DFM
DFM is where many projects either stay on track or begin slipping. A buyer changing wall thickness after steel cutting may trigger additional machining, delayed sampling, and new validation rounds.
One common example is an automotive supplier switching from ABS to PC/ABS after tooling starts because the original resin failed heat testing. That single material change can affect shrinkage rates, gating, and cooling behavior.
T1 y validación
After tooling is complete, the manufacturer runs the first trial shot, often called T1 sampling. Engineers inspect dimensions, cosmetic finish, gate marks, Flash, and cycle consistency.
Mass production should not begin immediately after T1 approval. Stable production requires process tuning, repeatability checks, and validated inspection procedures before the production ramp starts.
How do you choose the right plastic material?
Material selection affects strength, heat resistance, tooling wear, Tiempo de ciclo, and final part cost. Choosing resin based only on price often creates long-term production problems.
The right resin depends on the product’s environment, load requirements, appearance goals, y condiciones de producción. Polypropylene works well for flexible consumer parts, while polycarbonate provides stronger heat resistance and impact performance.
A resin also affects tooling life and production efficiency. Glass-filled materials can increase mold wear. High-temperature resins often require slower cycle times and more advanced tooling design. Grupo Goodfish explains how resin behavior directly impacts manufacturability and long-term part performance.
| Material | Mejor Uso | Beneficio clave | Limitaciones |
|---|---|---|---|
| PP | Bienes de consumo | Bajo coste, flexible | Menor resistencia al calor |
| ABS | Viviendas | Buena apariencia | Durabilidad moderada |
| PC | Electrónica | Alta resistencia al impacto | Mayor coste |
| Nailon | Componentes mecánicos | Resistencia al desgaste | Absorción de humedad |
The cheapest resin is not always the lowest total cost. A lower-grade material may increase defect rates, cosmetic rejection, or part failure during production.
A medical device project may require multiple resin evaluations before approval. If sterilization temperatures exceed the material’s limit, the part can warp or crack after shipment. En esos casos, engineering-grade resin becomes necessary even if tooling and cycle costs increase.
For broader mold and resin production context, véase Soluciones de moldes plásticos.
Should you use aluminum or steel tooling?
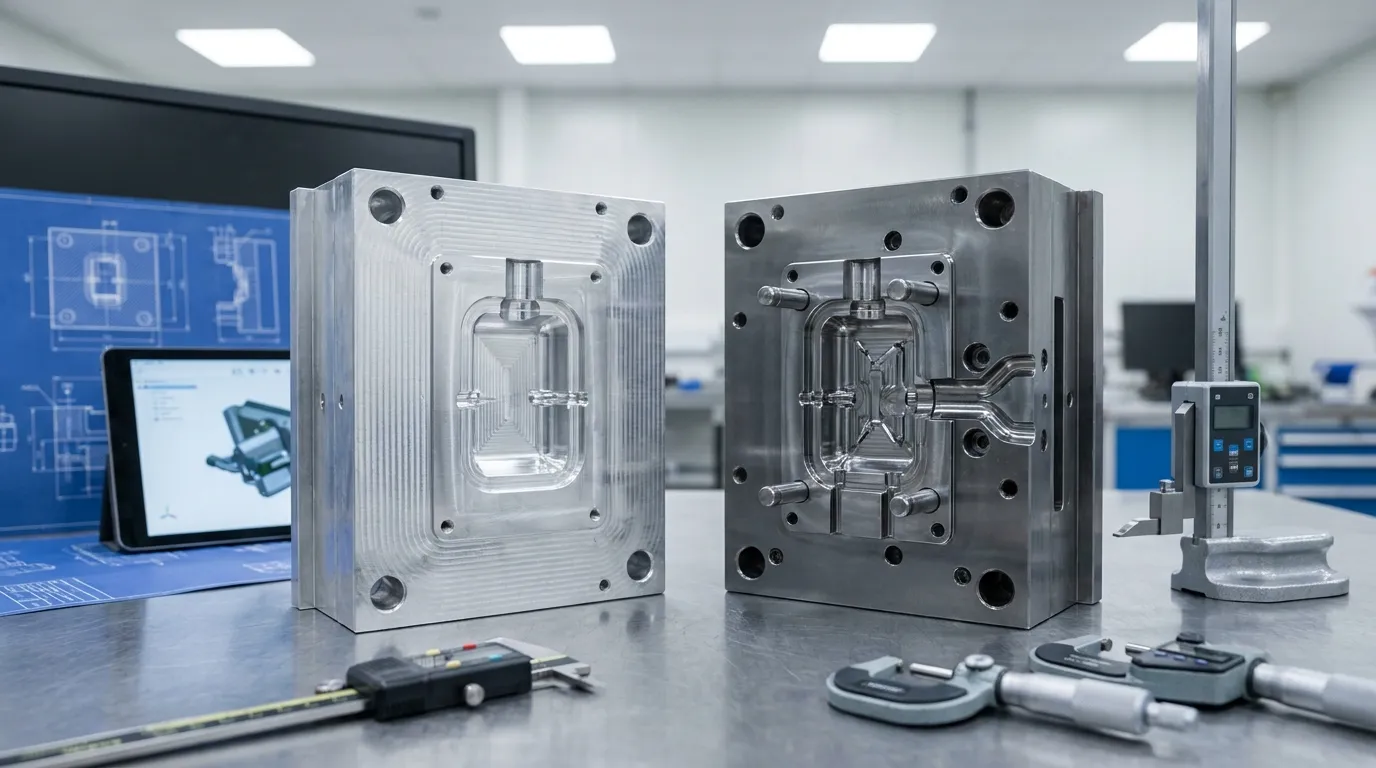
Aluminum molds reduce lead times and tooling cost for lower-volume projects, while hardened steel tooling is safer for long production runs and tighter tolerances.
Tooling material changes both project economics and production stability. Aluminum molds machine faster and cost less upfront, making them useful for prototyping, bridge production, or market testing.
Steel molds require more time and investment, but they handle higher production volumes and abrasive materials more reliably. Weilin Plastic notes that aluminum tooling is often preferred for low-volume manufacturing because of faster turnaround times.
Tabla de Decisión de Herramientas
| Factor | Herramientas de aluminio | Herramientas de acero |
|---|---|---|
| Tiempo de espera | Más rápido | Más largo |
| Coste inicial | Inferior | Más alto |
| Vida útil de producción | Inferior | Mucho más alto |
| Flexibilidad de revisión | Más fácil | Más difícil |
| Mejor para | Prototypes, bridge runs | Producción a largo plazo |
Aluminum tooling is not always the cheapest long-term option. It works well for startup launches and pilot production, but hardened steel tooling is safer when repeatability and large production runs matter.
A startup launching a smart home device may choose aluminum tooling for the first 8,000 Unidades. Once demand stabilizes, the company can transition to steel tooling for larger production volumes and improved durability.
If you're comparing tooling suppliers, Reseña Herramientas de moldes por inyección before committing to a production plan.
What affects tooling cost and production pricing?
Tooling cost depends on part geometry, Recuento de cavidades, resin behavior, Requisitos de tolerancia, y volumen de producción. Small design changes after tooling starts can increase both lead time and total project cost.
Most injection molding costs fall into two categories: tooling cost and per-part production cost. Tooling includes machining, mold design, steel selection, cooling systems, and finishing work. Per-part cost depends on resin usage, Tiempo de ciclo, labor, and output volume.
Complex geometry increases tooling cost quickly. Socavos, threaded sections, side actions, and polished cosmetic surfaces all require additional machining and engineering time.
| Factor de coste | Impacto en la fijación de precios |
|---|---|
| Molde de múltiples cavidades | Mayor coste de herramientas, lower part cost |
| Tolerancias estrictas | Más mecanizado y validación |
| Resina de grado ingeniero | Mayor coste de los materiales |
| Acabado cosmético | Pulido adicional |
| Revisiones de diseño | Retrasos y reestructuración |
The lowest mold quote is rarely the lowest total project cost. Weak DFM review and poor validation often create expensive corrections later.
Por ejemplo, a buyer approving tooling before finalizing snap-fit geometry may face steel modifications after T1 sampling. Even small tooling revisions can delay production schedules and increase engineering costs.
When evaluating suppliers, a qualified Proveedor de molduras personalizadas should explain cost drivers clearly instead of quoting only a single mold price.
How long does a custom injection molding project take?
Most custom plastic injection molding projects take several weeks to months depending on tooling complexity, Revisiones, sampling cycles, and production validation requirements.
Simple tooling projects may move from DFM approval to production in a few weeks. Complex hardened steel molds with multiple cavities and cosmetic requirements often take much longer. Según Aprios, production mold lead times can extend from several weeks to multiple months depending on complexity.
| Fase del proyecto | Sincronización típica |
|---|---|
| Análisis de DFM | 2-7 días |
| Mold design | 1-2 semanas |
| Fabricación de herramientas | Varias semanas |
| Muestreo T1 | Unos días |
| Revisiones y validación | Variable |
| Production ramp | Depende de la aprobación |
Causas comunes del retraso
Most delays come from project changes, not machine downtime. Late design revisions, Especificaciones incompletas, resin changes, and failed validation rounds create the largest schedule disruptions.
A medical device project may require multiple T1 sampling rounds before dimensional stability meets approval standards. That extra validation time is normal in regulated production environments.
Evokpoly also highlights how tooling complexity and engineering changes affect overall lead time.
What should happen during sampling and production validation?
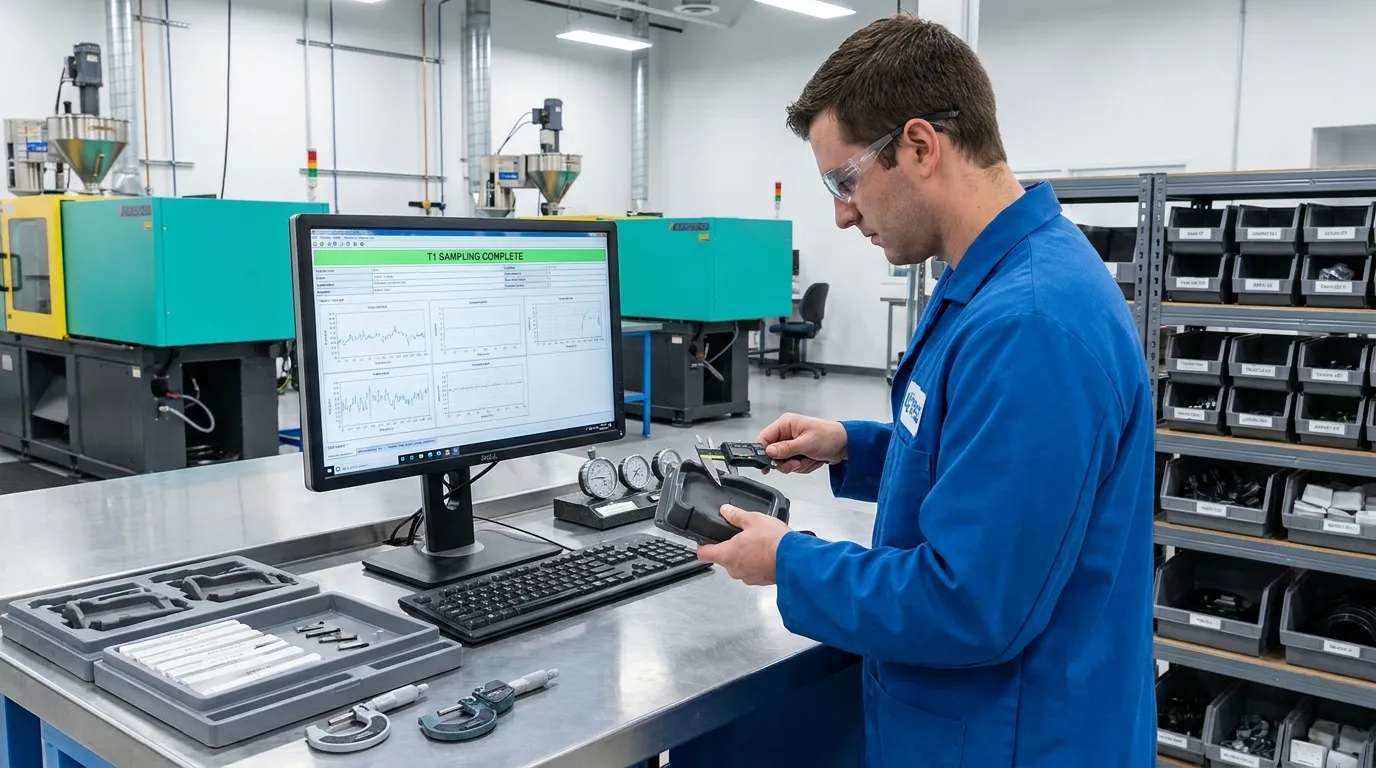
T1 sampling is where manufacturers validate dimensions, material behavior, and molding stability before full production begins. Skipping structured validation increases the risk of downstream defects and delays.
Sampling is the transition point between tooling completion and production readiness. The goal is not just to create acceptable parts. The goal is to prove the process can repeat stable results consistently.
Manufacturers usually inspect dimensions, Calidad cosmética, gate performance, cooling behavior, and material consistency during T1 and follow-up validation rounds.
Lista de verificación de preparación para la producción
- Aprobación de muestra T1
- Informe de inspección dimensional
- Verificación de resina
- Inspección de acabado superficial
- Revisión de parámetros de proceso
- Aprobación de envases
- Revisión de la planificación logística
- Confirmación de seguimiento de revisiones
A rushed production launch often creates avoidable quality problems. Faster production timing only helps if validation procedures are complete.
Before export shipment, some manufacturers also perform mold function testing and trial verification. Moho alpino recommends reviewing trial reports, functionality, and dimensional checks before shipment approval.
For additional production-stage planning, revisa el Proceso de validación de moldes used during mold qualification and production release.
How can buyers reduce production delays and supply chain risk?
Most production delays come from design revisions, Especificaciones incompletas, Cambios en las herramientas, and poor production planning rather than machine downtime alone.
The best way to reduce delays is to lock specifications before tooling begins. Changing geometry, resin type, or surface finish after steel cutting usually affects tooling, Validación, and scheduling.
International projects also require planning for customs paperwork, shipping schedules, and packaging requirements. Both Trade.gov y U.S. Customs and Border Protection provide guidance related to import procedures and shipment documentation.
| Si esto ocurre | Aumento del riesgo |
|---|---|
| Cambios de materiales tras el uso de herramientas | Retrasos en el muestreo |
| Especificaciones de tolerancia poco claras | Fallos en la inspección |
| Sin reseña de embalaje | Daños en el transporte marítimo |
| Cadencia de comunicación débil | Confusión en la producción |
A buyer delaying steel cutting until DFM approval often saves far more money than a buyer rushing into production. Early discipline reduces revision cycles and keeps production schedules predictable.
Las empresas que se preparan para la ampliación de la producción también deberían revisar Apoyo a la planificación de producción before approving long-term manufacturing agreements.
How do you choose the right injection molding manufacturer?
Choosing the right supplier depends on engineering support, quality systems, tooling capability, and communication quality. A manufacturer should help reduce production risk, not simply quote a mold price.
Buyers should evaluate whether the supplier handles DFM reviews, sampling reports, validation support, and export coordination internally. Clear engineering communication matters just as much as machine capacity.
Lista de verificación de evaluación de proveedores
- Soporte de ingeniería DFM
- Experiencia en herramientas
- Capacidad de producción
- Procedimientos de inspección de calidad
- Experiencia en exportación y logística
- Controles de abastecimiento de materiales
- Tiempo de respuesta en la comunicación
- Proceso de gestión de revisiones
An experienced supplier should also explain where risk exists. Por ejemplo, a supplier producing automotive parts may recommend hardened steel tooling immediately if annual production targets exceed projected aluminum mold lifespan.
If you're comparing long-term manufacturing partners, an Fabricante experimentado de moldes should be able to explain tooling decisions, validation methods, and production scalability clearly.
Acertando en el siguiente paso
A successful custom plastic injection molding project depends on early planning, realistic timelines, and disciplined validation. Buyers who focus only on mold price often face higher costs later through revisions, Retrasos, o producción inestable.
Start by reviewing your production volume, Requisitos de materiales, Expectativas de tolerancia, and launch timeline. Then evaluate whether aluminum or steel tooling fits the project long term. A supplier that supports DFM review, structured sampling, and production validation will usually reduce risk far more effectively than a low-cost quote alone.
Preguntas frecuentes
How much does custom plastic injection molding cost?
Costs depend on tooling complexity, resin selection, Recuento de cavidades, Requisitos cosméticos, y volumen de producción. The mold is usually the largest upfront expense, while per-part pricing becomes lower as production volume increases.
How long does it take to build an injection mold?
Simple molds may be completed within a few weeks, while complex hardened steel tooling can take several months. Rondas de muestreo, Revisiones, and validation requirements also affect the final production timeline.
¿Deberían las herramientas estar hechas de aluminio o acero??
Aluminum tooling works well for prototypes and lower-volume production because it reduces cost and lead time. Steel tooling is better for large production runs, Tolerancias más estrictas, and longer mold lifespan.
Which plastic material should I use for my application?
Material selection depends on heat resistance, Durabilidad, Flexibilidad, Exposición química, and cosmetic requirements. Resin choice also affects tooling wear, Tiempo de ciclo, and long-term production consistency.
What certifications should I look for in an injection molding supplier?
Most buyers evaluate ISO compliance, quality management procedures, traceability systems, and industry-specific certifications. Medical and automotive programs often require stricter validation and inspection standards.
What causes delays in injection molding projects?
Revisiones de diseño tras el inicio de la herramienta, Especificaciones incompletas, material changes, and failed validation rounds are common delay sources. Early DFM review helps reduce many of these production risks.
Compartir:



Escrito por Sunshine
Al sol, Somos un fabricante y proveedor profesional de componentes de moldes de precisión, ofreciendo una amplia gama de productos para aplicaciones de estampado y moldes de inyección. Nuestro enfoque principal es el punzonamiento de troqueles, Pasadores y fundas eyector, y postes guía y casquillos. Con mecanizado CNC avanzado, Control de calidad estricto, y una fuerte capacidad de producción, Garantizamos la fiabilidad, Piezas de alta precisión, junto con componentes estándar en stock para un suministro global rápido y eficiente.
NOTICIAS
CONSIGUE EL SERVICIO
Con piezas de calidad para todos los presupuestos y personal amable formado para que tu visita sea informativa y sin complicaciones.
