



Heat Treatment for Mold Parts: Dureza, Resistencia al desgaste, and Tool Life
Heat treatment for mold parts improves hardness, Resistencia al desgaste, and tool life by changing the steel structure and stabilizing high-friction surfaces. Processes like quenching, tempering, and nitriding help ejector pins, puñetazos, Postes guía, and sleeves resist wear, Grietas, y deformación. The right treatment depends on the mold component, cycle volume, operating stress, and dimensional tolerance requirements.
Mold components fail faster when heat treatment doesn't match the material or production environment. A punch may crack because it's too hard. A guide bushing may lose alignment because it distorted during quenching. Choosing the right process helps reduce maintenance, improve cycle consistency, and extend mold life without increasing unnecessary tooling costs.
What does heat treatment do for mold parts?
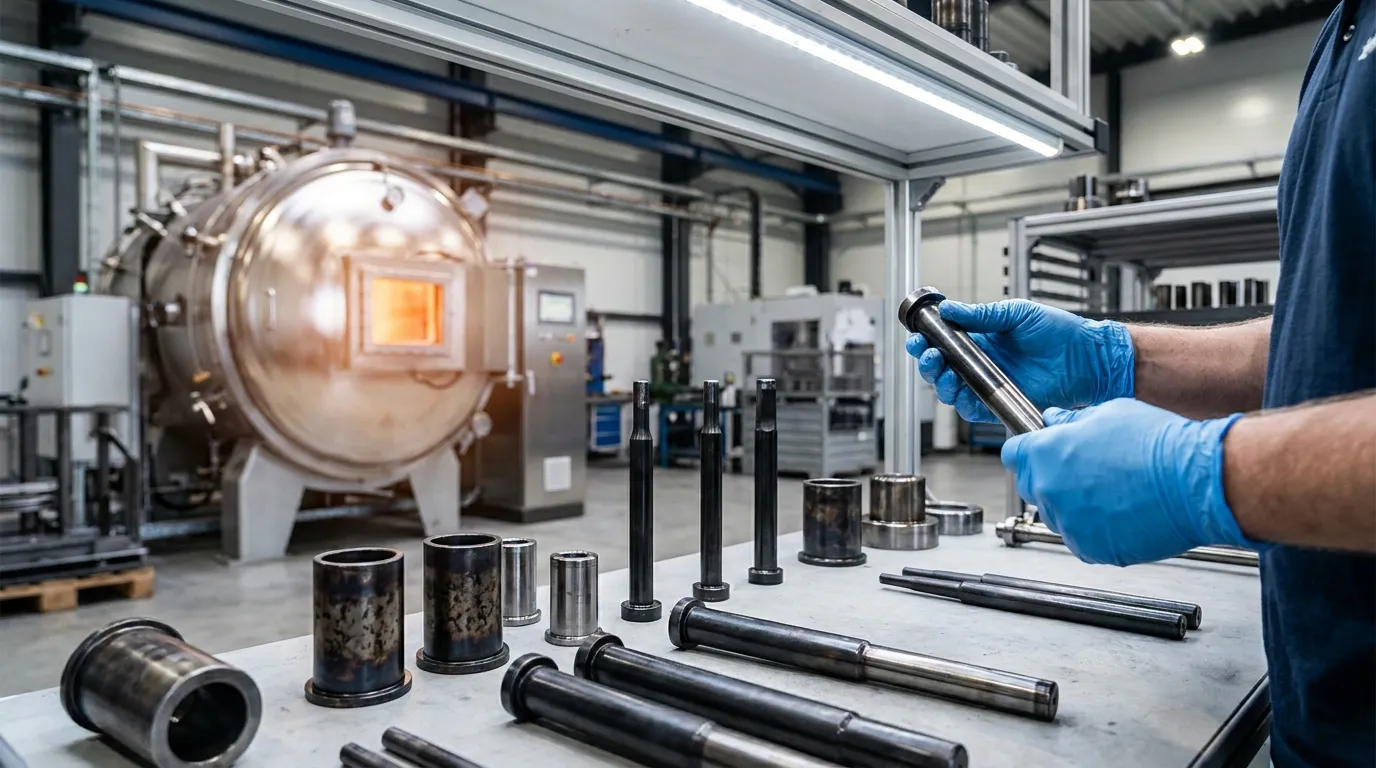
Heat treatment for mold parts improves hardness, Resistencia al desgaste, and dimensional stability by changing the steel microstructure. Proper treatment extends mold life and reduces maintenance, but excessive hardness can increase cracking risk.
Heat treatment controls how mold steel responds to stress, Fricción, and repeated production cycles. During processes such as quenching and tempering, the steel is heated and cooled under controlled conditions. This changes the internal grain structure and improves the part's mechanical properties.
In injection molds, high-contact components experience constant pressure and sliding movement. Ejector pins push parts out thousands of times per day. Guide posts absorb alignment stress during every cycle. Without proper heat treatment, these surfaces wear quickly and lose dimensional accuracy.
Según Guía para el tratamiento térmico al vacío, stress relief and controlled heating help reduce internal defects and improve stability. That matters because even small dimensional changes can affect mold alignment and surface quality.
Higher hardness is not always better. Some mold parts fail earlier because they become too brittle after aggressive hardening. In many production environments, balanced toughness and wear resistance perform better than maximum hardness alone.
| Objetivo del tratamiento térmico | Beneficio de la producción |
|---|---|
| Aumentar la dureza | Mejor resistencia al desgaste |
| Mejorar la tenacidad | Menor riesgo de grietas |
| Reducir el estrés | Mejor estabilidad dimensional |
| Endurecer superficies | Vida útil de los componentes más larga |
| Estabilizar la estructura | Precisión consistente en la producción |
Para una visión más amplia de la completa Componentes del molde de inyección, it's important to understand how each part handles different loads and wear conditions.
Which mold components benefit most from heat treatment?
High-friction mold components such as ejector pins, puñetazos, Postes guía, and sleeves benefit most from heat treatment because they face repeated wear, Presión, and alignment stress during high-cycle production.
Not every mold part requires the same treatment level. Structural plates may only need moderate hardness, while moving components often need stronger surface protection. The highest wear usually appears where metal-to-metal contact repeats continuously.
A high-cycle automotive mold is a good example. If ejector pins are too soft, the pin heads wear unevenly and start sticking inside the mold. That creates ejection problems, longer cycle times, and more maintenance shutdowns.
| Componente de molde | Tipo de esfuerzo principal | Enfoque recomendado |
|---|---|---|
| Pasadores eyectores | Desgaste deslizante | Dureza superficial |
| Puñetazos | Impacto y presión | Dureza de tenacidad |
| Bujes guía | Fricción de alineación | Resistencia al desgaste |
| Fundas | Movimiento repetido | Estabilidad superficial |
| Núcleos de molde | Calor y presión | Estabilidad dimensional |
Guide parts deserve special attention because alignment problems spread across the entire mold system. A distorted guide bushing can shift cavity positioning and increase flash defects. This is one reason heat treatment is closely tied to the overall Proceso de producción de moldes.
Medical molding applications often use nitrided sleeves because the process creates a hard outer layer without causing large dimensional changes. That helps maintain polished surfaces and consistent cavity performance over long production runs.
What hardness range is best for different mold parts?
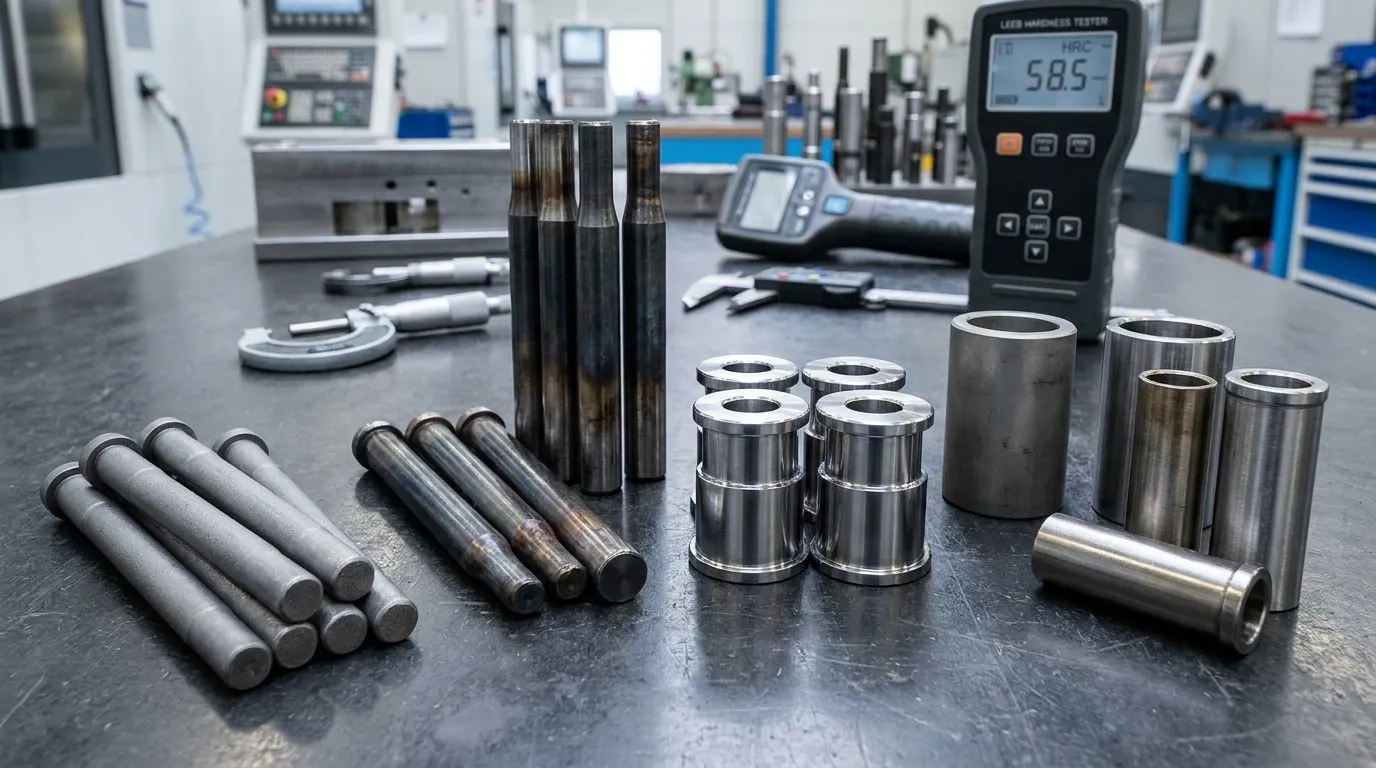
The best hardness level depends on the component function. High-wear parts often require higher hardness, while alignment and structural parts need more toughness to avoid cracking or deformation.
Many buyers assume harder mold parts automatically last longer. That isn't always true. A punch with excessive hardness may crack under repeated impact, especially in fast-cycle production. A slightly lower hardness range can improve toughness and extend usable service life.
The right balance depends on friction, impact load, thermal stress, and dimensional requirements. High-wear surfaces usually benefit from harder outer layers, while structural parts often need flexibility to absorb stress safely.
Tabla de decisión para el tratamiento térmico de componentes de moho
| Componente | Dureza recomendada | Tratamiento preferente | Riesgo principal de fallo | Mejor aplicación |
|---|---|---|---|---|
| Pasador eyector | HRC 58-62 | Nitruración | Desgaste superficial | Moldes de alto ciclo |
| Punch | HRC 56-60 | Temple de temple | Grietas | Impacto repetido |
| Buje guía | HRC 50-56 | Endurecimiento mediante | Distorsión | Sistemas de alineación |
| Manga | HRC 58-60 | Nitruración | Galling | Moldes de precisión |
| Núcleo de molde | HRC 48-54 | Tratamiento térmico al vacío | Fatiga térmica | Cavidades complejas |
Según Guía del proceso de tratamiento térmico al vacío, controlled cooling improves dimensional stability and reduces distortion risk. That's especially important for precision molds with tight tolerances.
A guide bushing that warps during quenching may still appear usable, but slight alignment changes can create uneven wear across the mold. Con el tiempo, that increases maintenance costs and reduces production consistency.
When should you use nitriding instead of through hardening?
Nitriding is often preferred for mold components that need high surface wear resistance with minimal distortion. Through hardening works better when uniform hardness is needed throughout the part.
The main difference is where the hardness is created. Through hardening affects the full thickness of the steel, while nitriding mainly hardens the outer surface. That makes nitriding useful for precision parts that must keep tight dimensional tolerances.
Nitriding also produces less deformation because it operates at lower temperatures than many quenching processes. In molds with polished sleeves or precision ejector systems, reduced distortion can improve long-term performance.
Beneficios de la nitruración para los pasadores eyectores
Ejector pins slide constantly during production. Nitriding creates a hard wear-resistant surface that reduces friction and slows surface damage. This helps prevent sticking and uneven wear patterns in high-cycle molds.
A nitrided sleeve used in medical molding may maintain surface quality much longer than a conventionally hardened sleeve. That matters when cavity finish directly affects cosmetic appearance or sealing performance.
Cuándo es más seguro el endurecimiento
Through hardening works better when the entire component must resist heavy mechanical load. Large punches and structural mold parts often need consistent hardness across the full section to avoid internal weakness.
Nitriding is not always the best choice. It works well for surface wear, but deeper impact loads may still damage softer internal material. En esos casos, through hardening provides more reliable structural support.
Elegir entre estos métodos debe alinearse con las condiciones de funcionamiento del molde y con su conjunto Directrices para el diseño de moldes. A process that performs well for guide sleeves may not work for impact-heavy punches.
How does poor heat treatment shorten mold life?
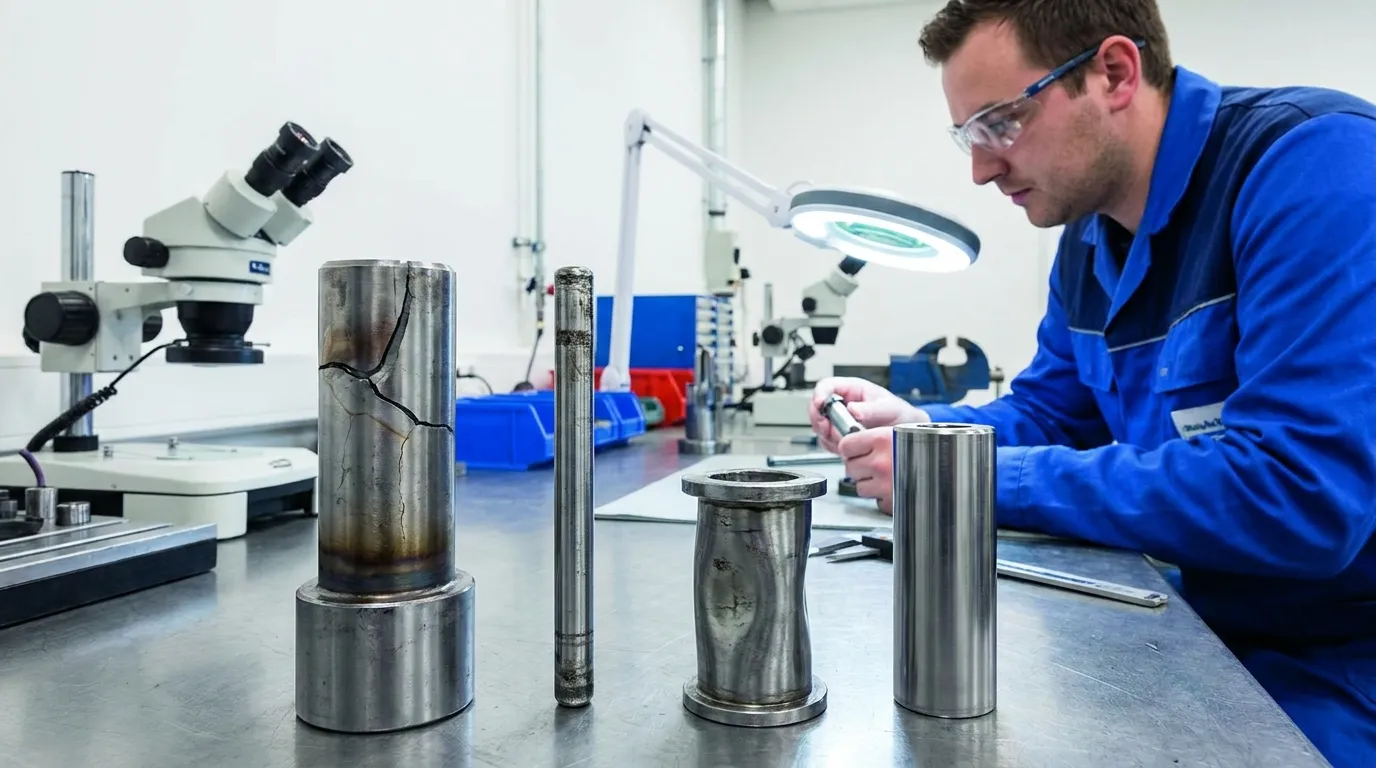
Poor heat treatment can shorten mold life by causing internal stress, Grietas, Distorsión, and unstable hardness. Many failures happen because the treatment process does not match the mold steel or operating conditions.
Heat treatment problems often appear slowly at first. A component may pass inspection but fail early during production because the internal structure isn't stable. Refrigeración desigual, excessive hardness, or poor stress relief are common causes.
One common failure involves over-hardened punches. In repeated stamping or molding cycles, the punch becomes brittle and develops surface cracks near high-stress corners. Once cracking starts, replacement usually becomes unavoidable.
Signos comunes de fallo en el tratamiento térmico
- Grietas superficiales alrededor de bordes o esquinas
- Patrones de desgaste desiguales en las piezas móviles
- Distorsión que afecta a la alineación del molde
- Reducción de la estabilidad al pulido
- Agallamiento prematuro o pegada
Según Guía del proceso de tratamiento térmico, cold treatment and stress reduction can help improve dimensional stability. Preventing distortion is especially important for guide systems and precision cavities.
Many mold failures blamed on poor steel quality are actually caused by incorrect cooling or uncontrolled heat treatment parameters. A guide bushing that loses alignment after quenching can create flash defects across the entire mold system, increasing long-term Costes de reemplazo de moho.
Lista de verificación de fallos en tratamientos térmicos
| Síntoma | Causa probable | Solución recomendada | Impacto en la producción |
|---|---|---|---|
| Grietas superficiales | Dureza excesiva | Objetivo de dureza inferior | Tiempo de inactividad inesperado |
| Distorsión | Refrigeración desigual | Temple controlado | Cuestiones de alineación |
| Desgaste rápido | Baja dureza superficial | Endurecimiento superficial | Mantenimiento frecuente |
| Galling | Acabado superficial pobre | Nitruración o pulido | Problemas de eyección |
| Puntos débiles | Calentamiento inconsistente | Revisión del control de procesos | Vida útil reducida de la herramienta |
How does heat treatment affect surface finish and maintenance?
Heat treatment directly affects friction, polishing stability, and long-term maintenance intervals. Poorly treated surfaces wear unevenly, lose polish quality faster, and create more production interruptions.
Mold surfaces with stable hardness usually maintain finish quality longer during high-cycle production. That becomes important in cosmetic molding applications where surface scratches or wear marks transfer directly onto the plastic part.
A properly nitrided sleeve may require fewer polishing cycles because the hardened surface resists abrasion better. Untreated or unstable surfaces often lose smoothness faster and increase drag during ejection.
Heat treatment also affects maintenance planning. Components with balanced hardness and toughness generally last longer between inspections, especially in molds running abrasive resins or continuous production schedules.
For molds where appearance matters, surface durability should align with the required Calidad de la superficie del molde. Heat treatment and polishing performance work together, especially in precision molding environments.
What should buyers ask before ordering heat-treated mold components?
Buyers should verify hardness range, Grado de acero, heat treatment method, and dimensional tolerance before ordering mold components. These details directly affect wear resistance, Frecuencia de mantenimiento, y estabilidad en producción.
Many sourcing problems start because the treatment process isn't clearly specified. Two components may use the same steel grade but perform very differently depending on how they were hardened and tempered.
Antes de aprobar la producción, buyers should confirm:
- Rango de dureza del blanco
- Método de tratamiento térmico utilizado
- Profundidad de tratamiento superficial
- Tolerancia dimensional tras el tratamiento
- Disponibilidad de inspección o certificación de dureza
A supplier should also explain whether the component uses nitriding, through hardening, vacuum treatment, or another process. That information matters because different methods affect distortion risk and maintenance intervals differently.
Por ejemplo, a high-cycle ejector system may need nitrided pins with controlled surface hardness, while a large structural punch may require deeper through hardening for impact resistance. Matching the process to the real production load helps prevent early failures and replacement costs.
Acertando en el siguiente paso
Heat treatment for mold parts affects much more than hardness. It influences wear resistance, alignment stability, Frecuencia de mantenimiento, y la consistencia de producción a largo plazo. A component that looks acceptable on paper may still fail early if the treatment process doesn't match the operating conditions.
The safest approach is to evaluate each mold component separately. Pasadores eyectores, Bujes guía, puñetazos, and sleeves all handle stress differently. Choosing the right heat treatment for mold applications helps reduce downtime, Extender la vida útil de la herramienta, and maintain stable molding performance over high production volumes.
Preguntas frecuentes
What is heat treatment in mold manufacturing?
Heat treatment changes the mechanical properties of mold steel through controlled heating and cooling. It improves hardness, Resistencia al desgaste, and dimensional stability so mold parts can handle repeated production cycles with less wear.
Does higher hardness always improve mold life?
Higher hardness does not always mean longer mold life. Excessive hardness can make mold components brittle and more likely to crack under impact or thermal stress during production.
What is nitriding in mold manufacturing?
Nitriding creates a hard wear-resistant surface layer by adding nitrogen to the steel surface. It's commonly used when mold parts need better wear resistance with minimal dimensional distortion.
Which mold parts usually require heat treatment?
High-wear mold components usually require heat treatment. Pasadores eyectores, puñetazos, Postes guía, Mangas, and wear surfaces face repeated friction and pressure during molding cycles.
What causes mold cracking after heat treatment?
Improper heat treatment can create internal stress that leads to cracking. Dureza excesiva, uneven cooling, poor material selection, and uncontrolled quenching are common causes.
How does heat treatment affect mold maintenance?
Correct heat treatment reduces maintenance requirements by improving wear resistance and dimensional stability. Mold components stay functional longer and need fewer replacements during high-cycle production.
Compartir:



Escrito por Sunshine
Al sol, Somos un fabricante y proveedor profesional de componentes de moldes de precisión, ofreciendo una amplia gama de productos para aplicaciones de estampado y moldes de inyección. Nuestro enfoque principal es el punzonamiento de troqueles, Pasadores y fundas eyector, y postes guía y casquillos. Con mecanizado CNC avanzado, Control de calidad estricto, y una fuerte capacidad de producción, Garantizamos la fiabilidad, Piezas de alta precisión, junto con componentes estándar en stock para un suministro global rápido y eficiente.
NOTICIAS
CONSIGUE EL SERVICIO
Con piezas de calidad para todos los presupuestos y personal amable formado para que tu visita sea informativa y sin complicaciones.
