



Tolerancia de pasadores de posicionamiento del molde para alineación repetible
There is no single mold positioning pin tolerance that works for every mold. Repeatable alignment depends on a complete tolerance chain: the pin diameter, the mating hole or bushing diameter, the fit between them, the position and orientation of both features, and the dimensional changes that occur during operation.
A pin can be ground to a very tight diameter tolerance and still fail to locate the mold correctly if its hole is misplaced, its axis is tilted, or two locating pins create an overconstrained pattern. For broader guidance on guide systems, Desgaste, and fit selection, véase Pasadores y casquillos de molde (Inferido). This guide focuses specifically on defining, calculating, documenting, and inspecting positioning-pin tolerances.
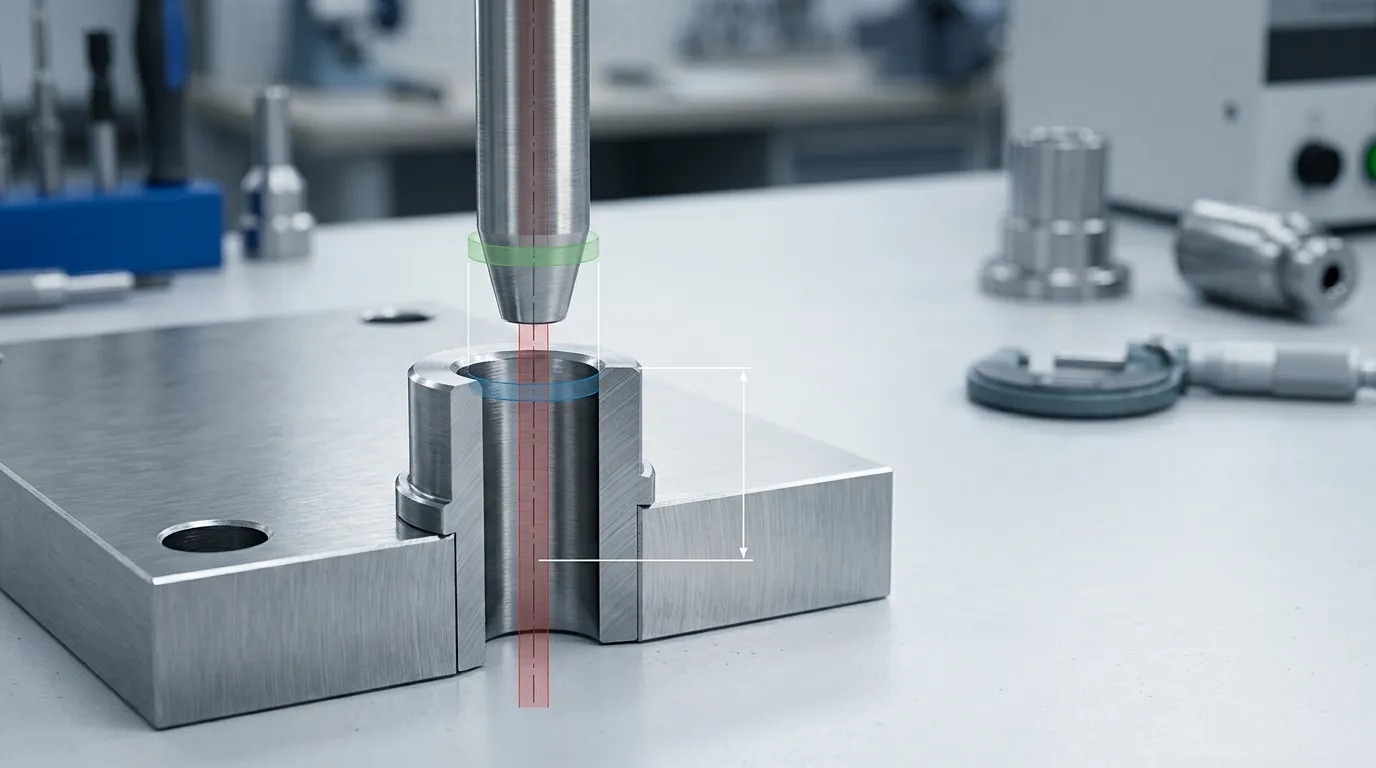
What Does a Mold Positioning Pin Tolerance Actually Control?
The word “tolerance” may refer to several different requirements. These controls are related, but they are not interchangeable.
| Control | Qué define | Lo que no define |
|---|---|---|
| Tolerancia al tamaño del pin | El diámetro de pasador aceptable más grande y menor | La posición del eje del pin |
| Tolerancia de agujero o casquillo | El mayor y el más pequeño ejemplares aceptables | Si el tubo está correctamente ubicado |
| Ajuste pasador-agujero | El posible espacio o interferencia entre ambas características | Error total de alineación del molde |
| Tolerancia geométrica | La posición y orientación permitidas del eje del pasador o agujero | El espacio real entre las piezas |
| Repetibilidad del sistema | Con qué consistencia el moho vuelve a la misma posición | Si esa posición repetida es la posición nominal correcta |
El Sistema ISO 286-1 de límites y ajustes defines size tolerances and fit relationships for holes and shafts. It does not control where a hole is located or whether its axis is perpendicular to the mold plate. Those requirements need geometric controls, such as those defined by ISO 1101.
Size Tolerance, Ajuste, and Alignment Are Different Requirements
Suppose a positioning pin and its mating hole are both within their specified diameter limits. That confirms only that their sizes are acceptable.
It does not confirm that:
- the pin and hole centers coincide;
- their axes are parallel;
- two locating holes have the correct spacing;
- the mold returns to its intended position;
- the assembly will still engage after heating or wear.
The actual fit comes from the combination of both size ranges. The smallest permitted hole paired with the largest permitted pin creates the tightest possible assembly. The largest hole paired with the smallest pin creates the loosest possible assembly.
Both extremes must be checked.
Posición, Orientación, and Repeatability Complete the Specification
A bore may have the correct diameter but still be offset from its basic location. A pin may be positioned correctly at the plate surface but tilted enough to bind over a long engagement length.
A complete positioning specification may therefore need:
- a functional datum reference frame;
- basic dimensions locating the pin or hole;
- positional tolerance;
- perpendicularity or another orientation control;
- pattern control for multiple locating features.
Repeatability and accuracy should also be distinguished. Repeatability describes how consistently the mold returns to the same position. Accuracy describes how close that position is to the intended nominal location.
A locating system can be repeatable but consistently offset if the feature pattern was manufactured in the wrong position.
Los pasadores de posicionamiento no deben tratarse automáticamente como equivalentes a Pasadores guía de molde. Guide pins primarily control movement as mold halves open and close. A dedicated positioning pin may establish a more precise final location after the mold halves approach engagement.
Define el requisito funcional antes de seleccionar el ajuste
A tolerance should start with the required function, not with a familiar fit designation.
Before assigning limits, Define:
- The maximum permitted translational alignment error.
- The maximum permitted angular error.
- The nominal pin diameter and engagement length.
- Whether the pin is permanent, removable, or replaceable.
- How often the mold will be assembled or disassembled.
- Which side retains the pin.
- Which side provides the locating engagement.
- The operating temperature range.
- The expected wear, Lubricación, and contamination conditions.
- The manufacturing and inspection methods available.
- Whether binding or excess clearance creates the greater functional risk.
A positioning system used for a removable insert may prioritize easy engagement and interchangeability. A permanently installed locator may require stronger retention on its mounting side. A heated mold may need enough room for differential thermal expansion between the pin, Bujes, and mold plate.
Application labels alone do not determine the correct fit. An “automotive mold” or “medical mold” still needs a defined alignment requirement, material combination, temperature range, y plan de inspección.
Separa la interfaz fija de la interfaz de localización
The two ends of a positioning pin usually perform different jobs.
| Interfaz | Función primaria | Posible dirección de ajuste |
| Lado de montaje | Mantener el pasador en la placa de soporte y conservar su eje | Controlled transition or interference, depending on design |
| Lado de localización | Entra en el agujero de acoplamiento o en el casquillo y limita el movimiento relativo | Controlled clearance or transition, depending on function |
Using the same fit on both sides can create avoidable problems. A locating-side interference fit may prevent normal assembly. Excessive mounting-side clearance may allow the pin to shift or loosen.
The final selection must also consider plate thickness, surrounding material, Método de eliminación, replacement needs, and the risk of distortion during installation.
Elige el ajuste y calcula la altura real
Autorización, Transición, and interference fits describe the relationship between the complete pin and hole tolerance zones.
Autorización, Transición, and Interference Serve Different Functions
| Tipo de ajuste | Resultado dimensional | Uso funcional típico | Riesgo principal |
| Ajuste de espacio | El agujero más pequeño sigue siendo más grande que el pasador más grande | Acoplamiento deslizante o desmontable | Movimiento excesivo si el espacio libre es demasiado grande |
| Transition fit | Some valid combinations have clearance; others have interference | Ubicación cercana o retención moderada | Fuerza de ensamblaje variable |
| Interference fit | El pasador más pequeño sigue siendo más grande que el agujero más grande | Retención permanente o semipermanente | Distorsión, Retirada difícil, o daños en la instalación |
These categories describe outcomes, not universal recommendations. A clearance fit may be suitable on the locating side while an interference or transition fit is used on the mounting side.
The hole-basis system is common because standard hole-making tools can establish a defined hole tolerance while the shaft or pin tolerance is selected to create the required fit. Aun así, a designation such as H7/g6 or H7/m6 is incomplete without the nominal diameter and governing standard. The numerical deviations change across diameter ranges.
Utiliza dimensiones límite para comprobar ambos extremos del ensamblaje
Calculate the limits before approving the fit.
Espacio mínimo
Minimum clearance = Smallest permitted hole − Largest permitted pinMáxima altura libre
Maximum clearance = Largest permitted hole − Smallest permitted pinA negative result represents interference.
Consider a hypothetical example:
| Característica | Diámetro mínimo | Diámetro máximo |
| Localización del agujero | 10.010 mm | 10.018 mm |
| Pasador de posicionamiento | 9,998 mm | 10.004 mm |
The tightest possible assembly is:
10.010 − 10.004 = 0.006 mm minimum diametral clearanceThe loosest possible assembly is:
10.018 − 9.998 = 0.020 mm maximum diametral clearanceThese values are examples only. They are not recommended SunshinePro specifications or universal mold tolerances.
Diametral clearance also should not be treated as the complete alignment error. In an ideal single-pin interface, the pin center may move radially by up to approximately half the diametral clearance before contact. The actual mold position also depends on the second locator, feature positions, axis angles, engagement lengths, Deformación, y condiciones de funcionamiento.
Control the Locating Pattern, Not Only the Pin Diameter
A precision fit cannot compensate for an incorrectly located pattern.
The pin and mating feature must be controlled from datums that represent how the mold is assembled and functions. These may include a seating face, a side reference, or another stable mold-base feature.
Use Functional Datums, Posición, and Axis Control
A practical drawing should identify:
- the surfaces establishing the functional datum reference frame;
- the basic locations of the pin and mating hole;
- the permitted positional variation;
- any required perpendicularity or axis-orientation control;
- the relationship between multiple locating features.
ISO 5458 provides complementary rules for pattern specifications under the ISO GPS system. Drawings using ASME conventions should follow ASME Y14.5.
The drawing should clearly use one governing convention. Mixing ISO and ASME symbols or assumptions without clarification can create conflicting interpretations between the designer, manufacturer, and inspector.
Evita la sobrelimitación con un par de bolas redondas y relevadas
Two fully round pins entering two close-fitting round holes can overconstrain the assembly.
For both pins to engage, the distance between the pins must agree closely with the distance between the mating holes. Even when every individual diameter is acceptable, accumulated spacing and position variation can cause binding.
A common locating arrangement uses:
- one round pin as the primary locator;
- one diamond, aliviado, or flattened pin as the secondary locator.
The round pin controls movement in two planar directions. The relieved pin controls the required secondary direction while allowing some variation along the relieved axis.
The secondary pin must be oriented correctly. Rotating its relieved direction by 90 degrees changes which movement it permits and which movement it controls.
Locator spacing also affects angular definition. Greater spacing can reduce angular movement for a given amount of linear clearance, but no universal spacing rule applies. Tamaño de la placa, Cargas, available space, hole-position capability, and engagement geometry still need evaluation.
Construir una pila de tolerancias en el peor de los casos para alineación repetible
The fit calculation covers only one part of the positioning system. A complete tolerance budget should include every variation capable of moving, tilting, or preventing engagement between the mold halves.
Typical contributors include:
| Colaborador | Posible efecto |
| Diámetro del pin | Cambios de liberación o interferencia |
| Agujero o tubo de casquillo | Cambios de liberación o interferencia |
| Posición de montaje del pasador | Mueve el eje localizador |
| Posición del agujero de unión | Mueve el eje receptor |
| Orientación del eje | Crea desajustes angulares o contacto con los bordes |
| Ajuste del diámetro exterior del casquillo | Permite o restringe el movimiento del casquillo |
| Relación aburrida hacia fuera | Desplaza el diámetro funcional del casquillo |
| Espaciado por patrón de pasadores | Afecta al compromiso simultáneo |
| Temperatura de la placa del molde | Cambia las dimensiones del componente |
| Desgaste | Aumenta la distancia efectiva |
| Escombros | Reduce el espacio libre para usar o impide que se sientan todos |
| Measurement uncertainty | Reduce la confianza en la decisión de aceptación |
A practical worst-case process is:
- Define the maximum permitted alignment variation.
- Identify each dimensional and geometric contributor.
- Calculate the tightest and loosest component fits.
- Add the possible positional and orientation effects.
- Check whether every permissible combination can assemble.
- Reserve allowance for operating temperature, Desgaste, and contamination.
- Confirm that the inspection system can verify the specified limits.
Worst-case analysis is appropriate when assembly must be guaranteed at every permitted limit. Statistical tolerance analysis may be useful in established, capable production processes, but it should not replace functional verification without a justified process model.
Variación de fabricación separada de la variación operativa
Manufacturing variation includes:
- component diameter;
- Diámetro del agujero;
- Posición en la característica;
- Perpendicularidad;
- pattern spacing;
- bushing installation position.
Operating variation includes:
- Expansión térmica;
- Desgaste;
- Escombros;
- Condición de lubricación;
- plate movement or deformation.
A fit that works during inspection at room temperature may become too tight after heating. A fit that begins with acceptable clearance may lose repeatability as the pin or bushing wears.
Lubrication can reduce friction and seizure risk, but it cannot correct an invalid tolerance stack. Material and hardness affect how well the components retain their dimensions over time, but those decisions should remain separate from the basic fit calculation.
Utiliza una pila hipotética para probar el diseño
Assume a design permits 0.030 mm of total lateral variation at a functional location.
A simplified hypothetical budget might allocate:
| Colaborador | Efecto permitido |
| Movimiento radial de pasador a casquillo | 0.008 mm |
| Variación de la posición de los pasadores | 0.006 mm |
| Variación de la posición del casquillo | 0.006 mm |
| Efecto de orientación y compromiso | 0.004 mm |
| Tolerancia por temperatura y desgaste | 0.004 mm |
| Margen de diseño restante | 0.002 mm |
If the calculated worst-case total exceeds 0.030 mm, the design must change. Possible actions include:
- reducing maximum clearance;
- improving positional control;
- increasing locator spacing;
- using a replaceable bushing;
- revising the relieved-pin geometry;
- reducing operating variation;
- redefining the functional requirement.
The example demonstrates the budgeting method only. Real values must come from the mold’s geometry, Condiciones de funcionamiento, and manufacturing capability.
Especifica claramente el requisito en el dibujo o en la RFQ
A supplier cannot reliably manufacture or inspect an ambiguous precision requirement.
The drawing or request for quotation should identify:
- nominal pin, hole, and bushing dimensions;
- limit dimensions or an unambiguous fit designation;
- the governing tolerance standard;
- separate mounting-side and locating-side requirements;
- Datos funcionales;
- basic feature locations;
- position and orientation tolerances;
- primary and secondary locator roles;
- the orientation of any relieved or flattened pin;
- material and hardness where functionally necessary;
- Condición de tratamiento térmico;
- surface finish on locating diameters;
- operating temperature assumptions;
- whether components must be interchangeable;
- whether selective assembly is permitted;
- required inspection characteristics;
- required inspection records;
- whether pins and bushings are supplied as matched components.
The supplier should also know which characteristics are function-critical. A tight pin diameter may be less valuable than a slightly wider size tolerance combined with better positional control.
Evita notas de precisión ambiguas
Specifications that need clarification include:
- “high-precision pin” without dimensional limits;
- “±0.005 mm” without naming the controlled feature;
- an ISO fit class without a nominal diameter;
- pin diameter tolerance without a mating-hole tolerance;
- diameter controls without feature-position controls;
- room-temperature dimensions without relevant operating conditions;
- a tolerance with no defined inspection method;
- “100% inspection” without identifying the inspected characteristics.
A numerical tolerance has meaning only when the feature, Fecha, Estándar, conditions, and measurement method are clear.
Verify the Pin, Hole, Pattern, and Assembly
Inspection should follow the structure of the specification.
| Requisito Controlado | Dirección adecuada de verificación |
| Diámetro del pin | Mide en ubicaciones y orientaciones definidas |
| Diámetro del agujero o del casquillo | Verifica los límites del diámetro con un método calibrado adecuado |
| Posición del pasador o agujero | Medición relativa al sistema de referencia de datos indicado |
| Orientación del eje | Verificar la perpendicularidad o la relación angular |
| Espaciado de patrones | Mide la relación entre las características localizadoras |
| Enfrentamiento completo | Utiliza una comprobación controlada del conjunto o un medidor funcional cuando sea apropiado |
| Repeatability | Prueba el ensamblaje repetido bajo condiciones definidas |
No single measurement verifies every requirement.
A micrometer may confirm a pin diameter but cannot establish the pin’s position in the mold plate. A bore measurement may confirm hole size but not perpendicularity. A functional gauge may show that the current assembly engages, but it may not identify which individual feature is approaching its tolerance limit.
The inspection plan should also consider:
- instrument resolution;
- Estado de calibración;
- Accesorios;
- measurement temperature;
- accessibility of the feature;
- measurement uncertainty.
If the measurement uncertainty is too large relative to the tolerance, the conformity decision becomes unreliable. Component conformity also does not automatically prove long-term repeatability under heat, Desgaste, and repeated mold cycles.
Decide si se necesita una tolerancia estándar o personalizada
A standard pin or bushing is suitable when its published dimensions, Clase de tolerancia, Geometría, Material, and mounting configuration satisfy the calculated tolerance stack.
Customization may be justified when the design requires:
- a non-standard diameter or locating length;
- separate mounting and locating diameters;
- un hombro o reborde especial;
- a defined relieved-pin orientation;
- a specific material or hardness;
- a controlled surface finish;
- unusual retention or removal features;
- a tolerance not available in a standard series.
The decision should start with the functional requirement rather than an assumption that custom parts are automatically more precise. A custom pin still depends on the mating hole, Bujes, Sistema de fechas, y método de inspección.
SunshinePro states that it supplies mold components and supports non-standard accessories based on drawings or samples. Es Ubicación del casquillo guía del pasador page lists straight, flangeado, and custom structures, along with standard or customized sizes. Buyers comparing catalog and drawing-based options can also review the broader guidance on Piezas estándar de molde.
Antes de pedir, confirm which feature the supplier’s stated tolerance applies to, how it will be inspected, and whether the component must be interchangeable with other pins or bushings.
For a drawing-based review, provide the pin and mating-feature limits, datum scheme, Ajuste obligatorio, Condiciones de funcionamiento, material or hardness requirements, and inspection expectations through the Página de contacto de SunshinePro.
Compartir:



Escrito por Sunshine
Al sol, Somos un fabricante y proveedor profesional de componentes de moldes de precisión, ofreciendo una amplia gama de productos para aplicaciones de estampado y moldes de inyección. Nuestro enfoque principal es el punzonamiento de troqueles, Pasadores y fundas eyector, y postes guía y casquillos. Con mecanizado CNC avanzado, Control de calidad estricto, y una fuerte capacidad de producción, Garantizamos la fiabilidad, Piezas de alta precisión, junto con componentes estándar en stock para un suministro global rápido y eficiente.
NOTICIAS
CONSIGUE EL SERVICIO
Con piezas de calidad para todos los presupuestos y personal amable formado para que tu visita sea informativa y sin complicaciones.
