



Lista de verificación para inspección de pasadores de punzón para control de calidad entrante y rutinario
A punch pin inspection checklist should answer four questions: Is this the correct punch? Does it match the approved specification? Is it still fit for service? What action should follow the inspection?
This guide covers individual punch pins used in metal-stamping dies. Incoming QC verifies a newly supplied punch against the purchase order, Dibujado, revision, and required documentation. Routine QC checks whether a punch remains serviceable after production use, Reesmerado, a collision, or another abnormal event.
Punch pins work within a larger die system. Guides, Bujes, retainers, stripper components, La Autorización, and alignment can all influence punch condition. The broader roles of these components are covered in the Guía de componentes del chip (Inferido). Aquí, the focus stays on inspecting and dispositioning the punch pin itself.
No universal tolerance, inspection interval, or wear limit applies to every punch pin. Acceptance must be based on the approved drawing, purchase specification, control plan, or another documented requirement.
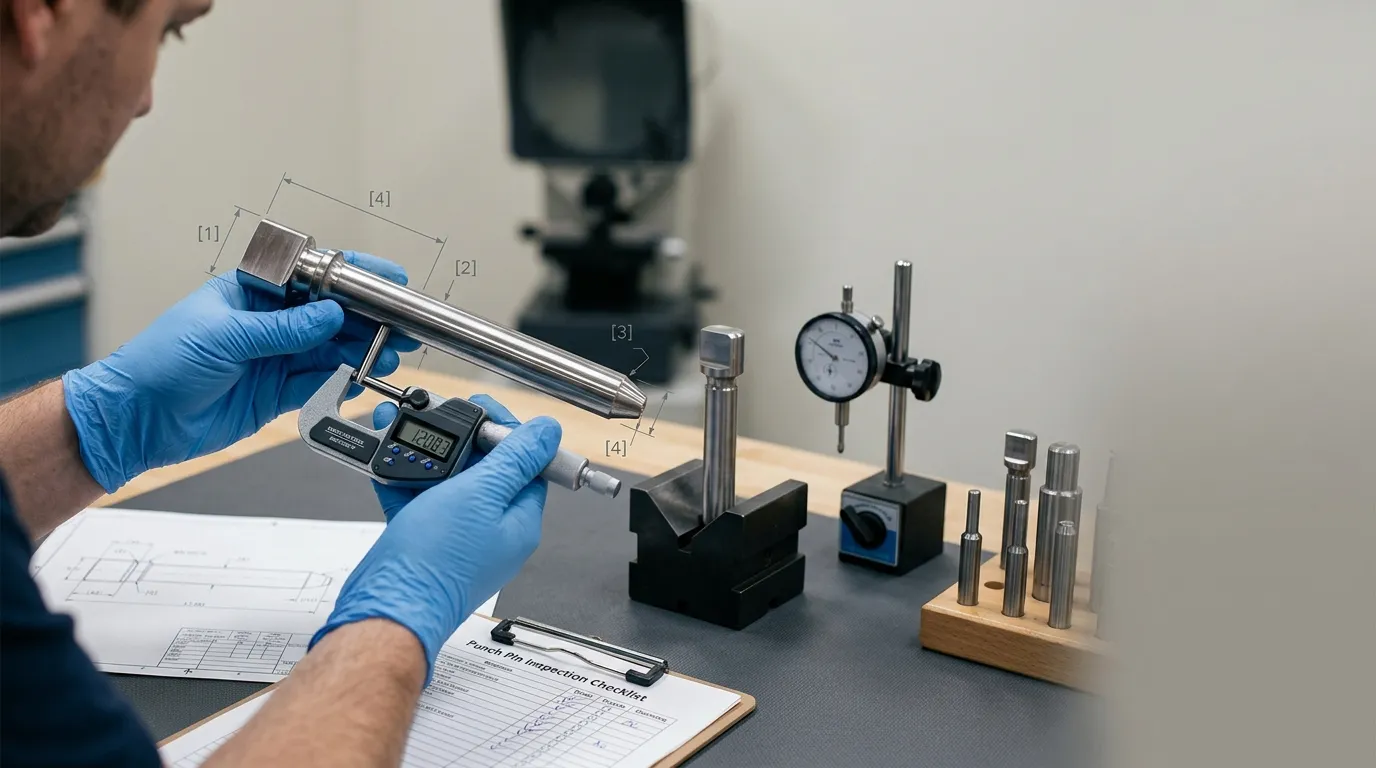
Controles de calidad entrantes y de rutina diferentes riesgos
Incoming and routine inspection use many of the same instruments, but they answer different questions.
| Fase de inspección | Propósito principal | Chequeos típicos | Decisión principal |
|---|---|---|---|
| Control de calidad entrante | Confirma que el punzón suministrado cumple con el pedido y la especificación aprobada | Part identity, Revisión del dibujo, material or coating documents, visible damage, Dimensiones, Geometría, inspection report | Accept, hold, return, or reject |
| Control de calidad rutinario | Confirma que un punzón usado sigue siendo seguro y funcional | Desgaste de los filos, grietas, Irritante, Cambio dimensional, Runout, Longitud de trabajo, Síntomas de producción, regrind history | Return to service, Monitor, regrind, reemplazar, or investigate |
| Inspección posterior al rectificado | Confirma que el afilado restauró el filo sin que otras características fueran inaceptables | Edge form, burr removal, Longitud total, Longitud de trabajo, Perfil, Condición de la superficie | Release, Reestructuración, o reemplazar |
| Inspección posterior al evento | Check for hidden or visible damage after a jam, Colisión, misfeed, or nearby breakage | Grietas, Flexión, head damage, Runout, Superficies de asientos, Componentes de acoplamiento | Cuarentena, Investigar, Reparación, o reemplazar |
Incoming inspection should establish a reliable baseline. Recording the punch’s as-received dimensions and condition makes later wear easier to identify.
Routine inspection compares the current punch against that baseline and any approved service limits. A punch can remain within its original manufacturing tolerance yet show an abnormal wear trend. Por el contrario, a worn feature may still appear visually acceptable while no longer meeting the documented service requirement.
Prepare the Punch, Documentos, and Measuring Equipment
Inspection should not begin with a caliper. It should begin with the correct documents, part identity, and measurement conditions.
- Confirm the inspection stage. Record whether the punch is incoming, in routine service, newly reground, or being checked after an abnormal event.
- Obtain the approved drawing. Verify the drawing number and revision before measuring anything. An accurate measurement against an obsolete revision is still an invalid inspection result.
- Review the purchase and quality requirements. Check the purchase order, control plan, approved sample, inspection-report requirement, and any requested material, Tratamiento térmico, Dureza, or coating documentation.
- Match the punch to its records. Confirm the part number, lot or serial number, Cantidad, material designation, coating designation, and any engraved identification.
- Inspect the packaging before cleaning. Record impact damage, Corrosión, broken protective packaging, loose punches, or signs that sharp edges contacted each other during transport.
- Clean the punch carefully. Quitar aceite, tierra, chips, and transferred material without rounding the cutting edge or scratching a coated surface. Residue on a diameter or seating face can affect the measurement.
- Stabilize the part when tolerances are tight. A punch arriving from a hot production area, cold warehouse, or vehicle may need time to reach the inspection environment. Temperature differences can affect dimensional results.
- Verify the measuring equipment. Check instrument identification, calibration status, measuring range, Resolución, Condición de contacto, and cleanliness. Confirm that any V-block, Centro, Calendario, or surface plate is also clean and suitable for the feature.
SunshinePro states that non-standard mold parts can be processed from customer drawings, while its punch-pin page lists diameter, Longitud, Estilo de cabeza, Calidad de material, and coating as customizable characteristics. Those fields should therefore be treated as drawing- and order-specific requirements rather than assumed product defaults.
Resolver especificaciones en conflicto o que faltan antes de la medición
Do not select a tolerance from memory, an old inspection sheet, or a generic catalog.
Place the punch on hold when:
- the drawing revision does not match the purchase order;
- the inspection report refers to another part or lot;
- the drawing and purchase specification contain conflicting limits;
- the material or coating designation is missing;
- the required datum or measurement method is unclear;
- an approved deviation is mentioned but not supplied.
Obtain written clarification from the responsible engineer, customer, or supplier before assigning a pass or fail result. The controlling-document hierarchy should follow the customer’s quality system or contract rather than an informal assumption.
Inspecciona cada característica del puñetazo en busca de daños visibles
Visual inspection is the fastest way to find obvious defects, but it should follow a consistent feature-by-feature sequence.
Use clean lighting and suitable magnification. Rotate the punch and inspect the complete circumference rather than viewing only one side.
| Zona de inspección | Condiciones a comprobar | Posible importancia | Siguiente acción típica |
| Filo y punta | Astillado, grietas, Redondeo de aristas, muelas, Deformación, Pastilla | Loss of cutting quality, Sobrecarga local, Impacto, Desgaste, adhesive material transfer | Medida, quarantine, regrind, o reemplazar |
| Vástago o cuerpo | Puntuación, Irritante, wear bands, Corrosión, Trastes, Material transferido | Poor guidance, Fricción, Desalineación, lubrication problem, Ajuste incorrecto | Limpio, measure diameter/runout, inspect mating parts |
| Cabeza y hombro | Crecimiento de setas, Aplastamiento, grietas, uneven seating marks, Deformación | Sobrecarga, incorrect seating, retainer problem, Apoyo insuficiente | Cuarentena e inspección del retenedor o del estado de los asientos |
| Radios de transición | Grietas, grinding marks, abrupt surface changes | Concentración de esfuerzos, Daño de molienda, fatigue initiation | Magnify, escalate, o reemplazar |
| Superficie recubierta | Peeling, Desprendido, arañazos, Decoloración, Sustrato expuesto | Coating damage, Fricción, Impacto, Corrosión, Desgaste | Record location, assess function, seek engineering review |
| Marcas identificativas | Missing or illegible part, lot, or serial information | Pérdida de trazabilidad o riesgo de mezclar revisiones | Esperar hasta confirmar la identidad |
A small chip at the cutting edge is not equivalent to a superficial scratch on a non-working surface. The inspection record should state the defect location, approximate extent, and whether it affects a functional feature.
Grietas, Deformación severa, or a damaged retention head generally justify immediate quarantine. Galling, Pastilla, or one-sided scoring may require inspection of the die system as well as the punch. Detailed causes of cracking and catastrophic failure belong in the guide to Rotura de punzones en troqueles de estampado.
Lo que la inspección visual no puede confirmar
Visual inspection cannot reliably establish:
- exact body or tip diameter;
- overall or working length;
- Rectitud;
- Runout, Concentricidad, or coaxiality;
- shaped-tip profile;
- numerical surface roughness;
- Calidad de material;
- heat-treatment conformity;
- Dureza;
- coating identity.
A punch may look undamaged but still be dimensionally out of tolerance. Grado de material, Dureza, and coating conformity may require traceable documentation or a specified test method.
Mide las dimensiones y geometrías que controlan el ajuste y la función
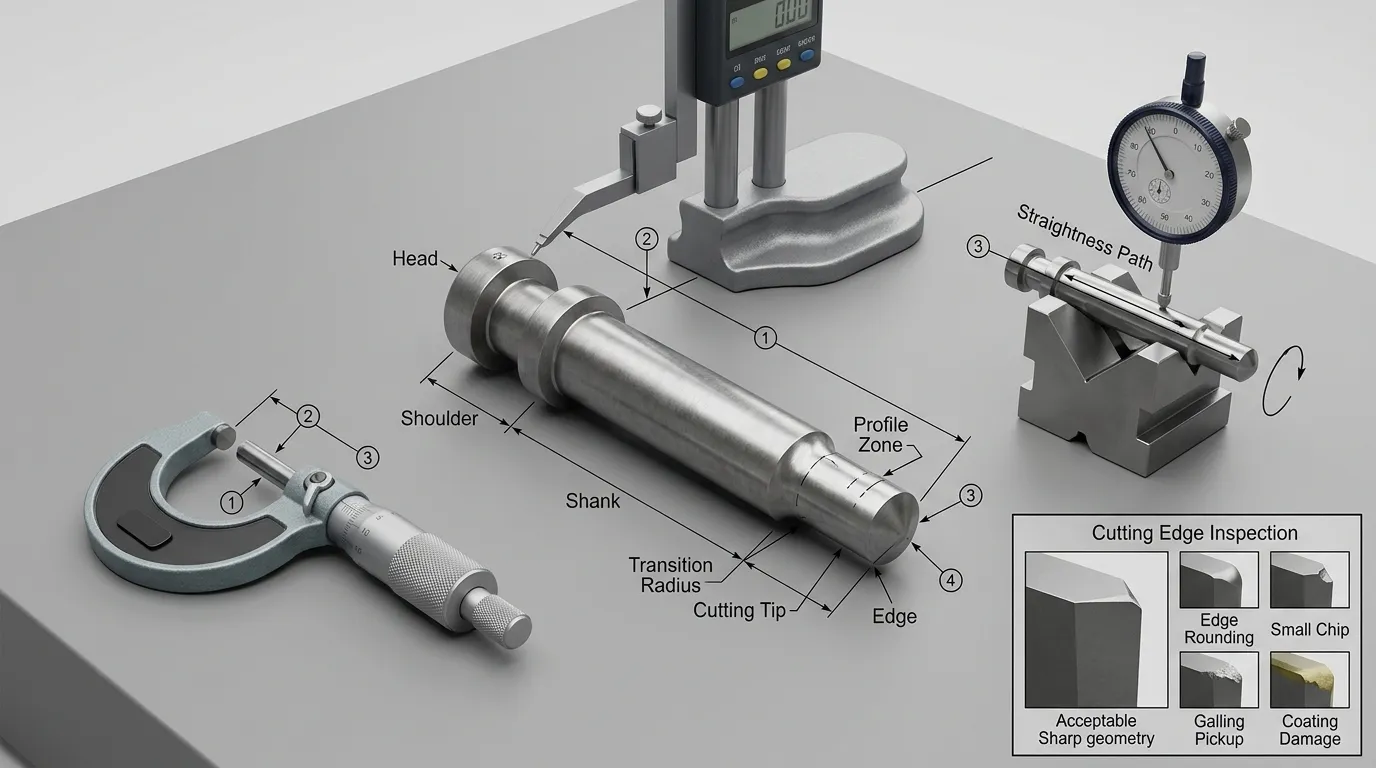
The approved drawing determines which dimensions and geometric controls must be inspected. Not every punch requires every measurement.
| Característica | Por qué es importante | Posible método de medición | Limitación significativa | Fuente de aceptación |
| Diámetro del cuerpo o del vástago | Affects guidance, Ajuste, Retención, y alineación | Outside micrometer; suitable limit gauge | Deben considerarse la ubicación del contacto y el taper | Especificación de dibujo o ajuste |
| Diámetro de la punta | Afecta al tamaño de la característica perforada y a la relación entre el puñetazo y el troquel | Micrometro, specialized gauge, optical system | Las puntas pequeñas o delicadas pueden no adaptarse a las lentillas estándar | Dibujo |
| Perfil de punta con forma | Controla agujeros no redondos o geometría formada | Optical comparator, vision system, CMM | Requiere una alineación correcta de los datos e interpretación del perfil | Dibujar con perfil requerido |
| Longitud total | Supports identification, installation, and regrind tracking | Height gauge, micrometer, Comparador, dedicated fixture | Las caras de los asientos deben estar limpias y estar referenciadas de forma consistente | Dibujo |
| Longitud de trabajo o proyección | Influye en la posición de operación y la penetración | Height gauge, Comparador, dedicated inspection fixture | Definition must match the drawing; do not borrow tablet-tooling terminology | Especificación de dibujo o configuración |
| Diámetro y grosor de la cabeza | Afecta a la retención y al asiento | Micrometro, caliper for screening, Comparador | Las muelas o el peening pueden distorsionar el contacto | Dibujo |
| Posición del hombro | Influencia en la colocación de asientos y la proyección ensamblada | Height gauge, Comparador, CMM | La configuración de datos debe reproducir el requisito de dibujo | Dibujo |
| Rectitud | Detecta flexión o desviación de eje | Indicator with suitable support, CMM, dedicated fixture | El método de soporte y la elección de datos afectan al resultado | Límite de servicio de extracción o aprobado |
| Esgotamiento circular o total | Muestra variación rotacional respecto a un eje de referencia | Indicator with centers or V-block; CMM | "Runout" debe coincidir exactamente con el control de dibujo | Dibujo |
| Concentricidad o coaxialidad | Evalúa la relación entre ejes o características | CMM o método especializado aprobado | No sustituyas una simple inspección de exención a menos que ingeniería la apruebe | Dibujo |
| Perpendicularidad | Afecta al asiento o alineación de las caras de los extremos y los hombros | Indicator, surface plate setup, CMM | Requiere una referencia de datos válida | Dibujo |
| Rugosidad superficial | Can influence friction, Ajuste, Lanzamiento, and galling | Probador de rugosidad superficial | Parámetro, corte, Dirección, and location must be specified | Dibujo o especificación de superficie |
| Dureza | Puede confirmar un requisito de tratamiento térmico | Prueba de dureza aprobada o documentación del proveedor | Test scale, Ubicación, Condición de la superficie, and indentation effect matter | Dibujo o especificación de materiales |
Geometric terms should be interpreted according to the drawing standard in use. ISO 1101 defines geometrical tolerancing concepts in the ISO system, mientras ASME Y14.5 is widely used for US-oriented GD&T drawings.
A drawing that specifies runout should not be rewritten as concentricity during inspection. These controls describe different requirements and may require different measurement strategies.
SunshinePro’s tungsten-carbide punch page lists micrometer or caliper checks, projector measurement, and roughness testing for that product category. Those published methods show the types of inspection that may be relevant, but they do not prove that every punch or every order receives the same checks.
Elige el instrumento según la tolerancia y la característica
Instrument choice should be based on the feature, Tolerancia, Acceso, and required measurement confidence.
| Instrumento | Mejor uso | Limitación principal |
| Micrometro | Diámetros y grosores externos accesibles | Contact geometry may not suit small, cónico, delicate, or irregular features |
| Pinza | Identification, broad dimensions, and screening | La resolución y la influencia del operador pueden no ser adecuadas para tolerancias estrictas |
| Medidor de altura y placa de superficie | Axial dimensions, shoulder positions, and comparative height checks | Requiere asientos controlados y configuración de datum |
| Indicador de caráter con bloque en V o centros | Runout, rotational variation, and some straightness checks | Los resultados dependen en gran medida de la posición de soporte y de la simulación de datos |
| Comparador óptico o sistema de visión | Profiles, Ángulos, Radios, tip shapes, and edge form | Requires alignment, magnification control, and correct profile interpretation |
| CMM | Geometría compleja y relaciones basadas en datos | Probe access, Accesorios, strategy, and uncertainty must be controlled |
| Medidor de go/no-go | Verificación funcional rápida de un límite de tamaño | Da información sobre aprobados/suspendidos pero no la desviación real ni la tendencia de desgaste |
| Probador de rugosidad | Verificación numérica de texturas superficiales | Requires the correct parameter, Dirección, corte, and measurement location |
Los manómetros de límite lisos están cubiertos por ISO 1938-1. A go/no-go gauge can be efficient for repeated checks, but variable measurement is still useful when the actual size or rate of wear matters.
Surface-texture requirements should be read from the drawing rather than inferred from appearance. ISO 21920-1 covers the indication of profile surface texture in technical product documentation.
Decide si el resultado es aceptable
A measured value is not meaningful until it is compared with an approved requirement.
Possible acceptance sources include:
- the current approved drawing;
- the purchase specification;
- the control plan;
- an approved customer deviation;
- an approved sample with defined measurement criteria;
- a documented service limit;
- a validated internal wear limit.
Nominal size alone does not determine acceptance. A drawing dimension of 10 mm, por ejemplo, cannot be judged without its tolerance and any related geometric or surface requirements.
Use a controlled decision process:
| Condición de resultado | Respuesta requerida |
| Claramente dentro del requisito | Registra el resultado y acepta o devuelve el punzón a servicio |
| Cerca de un límite o inconsistente | Verify cleanliness, Temperatura, Instrumento, method, Accesorios, datum setup, y repetibilidad |
| Fuera del requisito | Ponponle en cuarentena el ponzón y comienza el proceso de no conformidad aprobado |
| La especificación falta o es contradictoria | Sujeta el golpe hasta que recibas una aclaración por escrito |
| Defecto repetido tras el reemplazo o el rectificado | Investigar el sistema más amplio de matriz y las condiciones del proceso |
Measurement uncertainty becomes important near a specification limit. ISO 14253-1 provides decision rules for proving conformity or nonconformity while accounting for measurement uncertainty.
In practical terms, a borderline reading should not be accepted or rejected casually. Confirm that the instrument and method are capable of resolving the requirement, then apply the organization’s documented decision rule.
El muestreo o la inspección al 100% depende del riesgo y de los requisitos del contrato
The inspection quantity should be determined by:
- customer or contract requirements;
- characteristic criticality;
- lot size;
- supplier performance history;
- process capability;
- failure consequence;
- previous nonconformities;
- whether the result is needed for wear trending;
- the control plan.
A statement such as “100% inspected” should identify which characteristics were checked. It may mean every punch received an identification and visual check, while only selected pieces received complete dimensional inspection.
Go/no-go gauging may support rapid inspection of every piece, but it does not provide the variable data needed to evaluate size distribution or wear trends.
Utiliza la inspección rutinaria para controlar el desgaste antes de la avería
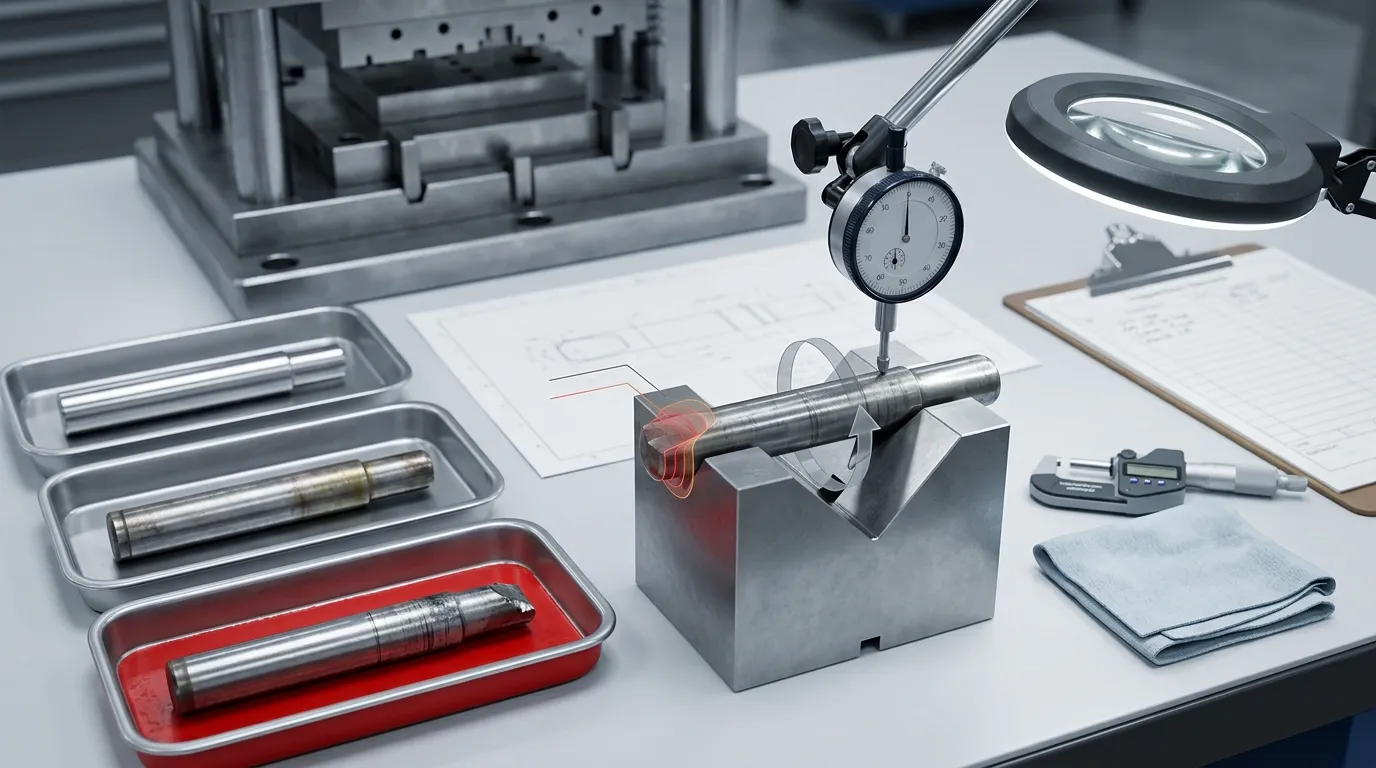
Routine QC should be based on risk and production history rather than one fixed interval for every punch.
Establish a baseline when the punch is first accepted, approved after setup, or returned from regrinding. Record dimensions and visible condition for the features most likely to change.
Trigger inspection when any of the following occurs:
- a planned production or maintenance interval is reached;
- the punch completes a high-risk or high-volume run;
- burr height or edge quality changes;
- stamped dimensions begin to drift;
- scratching or pickup appears on the part;
- stripping force increases;
- press load or operating sound changes;
- slug pulling or jamming occurs;
- a misfeed, Colisión, or material double-feed occurs;
- a nearby punch chips or breaks;
- the tool is removed for maintenance;
- Lubricación, stock material, or process settings change;
- the punch returns from regrinding.
Compare current values with the baseline and approved service limits. Trend data can reveal gradual wear before a dimension crosses a rejection limit.
Production symptoms should be treated as inspection triggers, not automatic diagnoses. Burrs may result from a worn punch, but they can also reflect die wear, Autorización, Alineación, work-material variation, or stripper problems. El Guía de troqueles de punzonados provides broader context on die materials, Tolerancias, Autorización, and system-level tooling considerations.
Verifica el punzón de nuevo después de volver a rectificar o de un evento anormal
A sharp edge does not by itself prove that a reground punch is ready for service.
Después de la rectificación, Comprobado:
- cutting-edge form;
- burr-free condition;
- Longitud total;
- working length or projection;
- tip diameter or profile;
- surface damage or overheating;
- remaining regrind allowance, where documented;
- identification and regrind history.
After a collision, misfeed, jam, or nearby breakage, also check:
- grietas;
- permanent bending;
- head or shoulder deformation;
- Runout;
- Superficies de asientos;
- guide and retainer contact;
- the mating die opening and surrounding components.
Do not return a punch to service solely because no visible crack is present. A collision can change alignment or runout without producing an obvious surface defect.
Registrar el resultado y asignar una disposición controlada
Inspection records should identify the punch, the requirement, the method, the result, and the final decision.
Como mínimo, Historial:
- Número de parte;
- Número de dibujo y revisión;
- proveedor;
- purchase order;
- lot or serial number;
- material and coating designation;
- inspection stage;
- characteristic inspected;
- specification and tolerance;
- measured result;
- instrument identification;
- inspector;
- inspection date;
- disposition;
- Notas, photographs, or defect location where useful.
Use a controlled disposition rather than an informal “looks okay” decision.
| Hallazgo | Posible distribución |
| Todas las características requeridas se ajustan | Aceptar o volver al servicio |
| El resultado es inconsistente o cerca de un límite | Limpio, stabilize, remeasure, or verify with a more capable method |
| Falta documentación | Espera o pon en cuarentena hasta que se presenten pruebas |
| Desgaste reparable de los bordes dentro de una margen aprobada | Solicita un rectificado aprobado por ingeniería |
| Crack, Astillas severas, permanent bending, or unsafe head damage | Reemplazar o rechazar |
| La dimensión está fuera del requisito | Cuarentena y proceso como no conforme |
| El mismo daño se repite repetidamente | Investigate clearance, Alineación, Orientación, Retención, Lubricación, y condiciones de proceso |
Nonconforming punches should be clearly identified and physically segregated so they cannot return to production accidentally.
SunshinePro states that its quality approach includes raw-material inspection, Monitorización en proceso, Pruebas finales, measuring equipment, and inspection reports. Buyers should still define the required inspection characteristics and documentation for each order rather than assume that one standard report fits every punch.
Qué pedir a un proveedor de pasadores perforadores
A buyer should define inspection evidence before the order is released, especially for custom or critical punches.
Request the items that are relevant to the application:
- Dibujo aprobado y revisión;
- part, lot, and serial identification requirements;
- drawing-specific inspection report;
- material certificate or certificate of conformity;
- heat-treatment or hardness evidence where specified;
- coating documentation where specified;
- Desviaciones aprobadas;
- packing and corrosion-protection requirements;
- identification of characteristics receiving 100% inspection;
- identification of characteristics inspected by sampling;
- measurement method for tight or complex tolerances;
- traceability between the punch, certificate, and inspection report.
Broad catalog statements are not a substitute for characteristic-level evidence. A supplier may state a general tolerance capability, but the buyer still needs confirmation that the required feature, Material, Geometría, and measurement method are suitable for the specific drawing.
SunshinePro lists tool steel, Acero de alta velocidad, carburo, Mecanizado CNC, Rectificado de precisión, EDM, Tratamiento térmico al vacío, and drawing-based customization on its punch-related pages. These published options can support an RFQ discussion, but the exact material, Proceso, Tolerancia, capa, and inspection documentation should be confirmed for the individual part.
Resumen de la Lista de Verificación de Inspección de Pasadores de Perforación
Use this condensed sequence for incoming, routine, post-regrind, and post-event inspections:
- Identify the inspection stage.
- Confirm the part number, lot or serial number, Dibujado, and revision.
- Review the purchase order, control plan, and document requirements.
- Inspect packaging and record transport damage.
- Clean the punch without damaging its edge or coating.
- Verify instrument condition, Distribución, Resolución, and calibration status.
- Inspect the cutting edge, Pista, Cuerpo, cabeza, Hombro, Radios, capa, and identification.
- Measure the dimensions and geometric characteristics required by the drawing.
- Use an instrument suitable for the feature and tolerance.
- Compare results with the approved acceptance source.
- Verify borderline results and account for measurement uncertainty.
- Record the specification, result, Instrumento, inspector, y fecha.
- Accept, hold, quarantine, regrind, reemplazar, or reject through a controlled disposition.
- Investigate the wider die system when the same damage repeatedly returns.
For a custom or replacement punch, submit the approved drawing together with the required material, capa, Inspección, and documentation needs. SunshinePro El Clavo de Perforación page provides its published product context, y la Página de contacto can be used to request drawing review or clarify inspection-report requirements.
Compartir:



Escrito por Sunshine
Al sol, Somos un fabricante y proveedor profesional de componentes de moldes de precisión, ofreciendo una amplia gama de productos para aplicaciones de estampado y moldes de inyección. Nuestro enfoque principal es el punzonamiento de troqueles, Pasadores y fundas eyector, y postes guía y casquillos. Con mecanizado CNC avanzado, Control de calidad estricto, y una fuerte capacidad de producción, Garantizamos la fiabilidad, Piezas de alta precisión, junto con componentes estándar en stock para un suministro global rápido y eficiente.
NOTICIAS
CONSIGUE EL SERVICIO
Con piezas de calidad para todos los presupuestos y personal amable formado para que tu visita sea informativa y sin complicaciones.
