



Pines de núcleo en moldeo por inyección: Cómo forman los agujeros y las características internas
Core pins injection molding systems use precision pins to create holes, Tragaperras, and internal features inside plastic parts. Molten resin flows around the pin during injection, leaving a finished void after cooling. Proper pin material, Apoyo, Balance de refrigeración, and tolerance control help prevent flash, hole distortion, Desgaste prematuro, and molded part defects. Stainless steel and carbide are common choices depending on resin type and production demands.
Small mold components often decide whether a molded part runs smoothly in production or creates constant quality problems. Core pins are a good example. A poorly supported pin can bend, wear out early, or produce inconsistent holes after thousands of cycles. A well-designed pin improves dimensional accuracy, extends mold life, and reduces downtime. Understanding how these pins work helps engineers and buyers avoid expensive tooling mistakes before production starts.
What are core pins in injection molding?
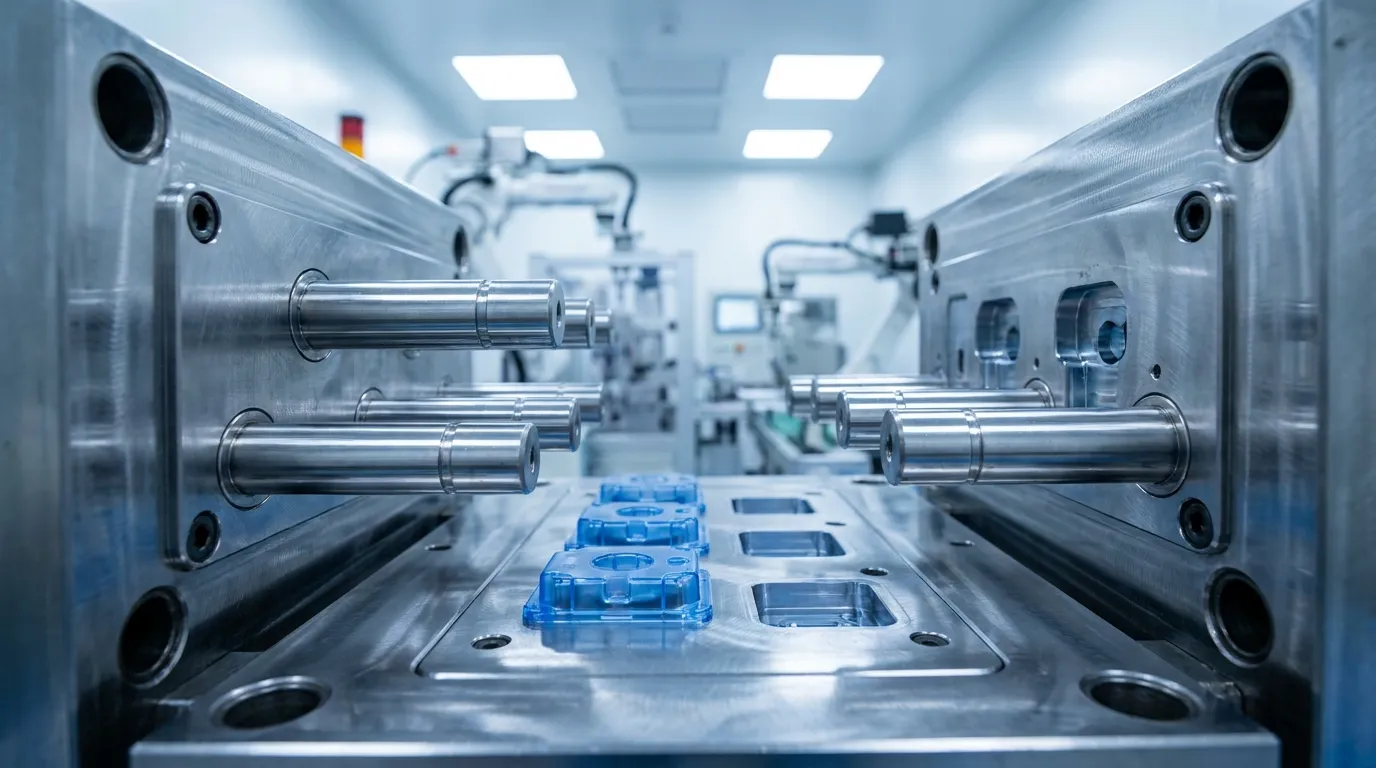
Core pins in injection molding are precision mold components used to create holes, Tragaperras, and internal features inside plastic parts. They stay fixed inside the mold while molten plastic flows around them during injection and cooling.
Core pins are usually installed inside the mold core or cavity area. Their job is simple: occupy space where plastic should not exist. When the part cools and ejects, the empty space left behind becomes a finished internal feature. Según DME, these pins are commonly used for precision molding applications where dimensional control matters.
Most core pins are made from hardened tool steel, Acero inoxidable, or tungsten carbide. The material depends on the resin being molded, expected production volume, and wear conditions. Glass-filled plastics, por ejemplo, can wear standard steel quickly because of their abrasive filler content.
Manufacturers also vary the shape and geometry depending on the part design. Some pins form simple round holes, while others create complex internal channels or narrow slots. High-volume molds often use replaceable Pines de núcleo de precisión so worn pins can be swapped without rebuilding the entire mold.
How do core pins form holes and internal features?
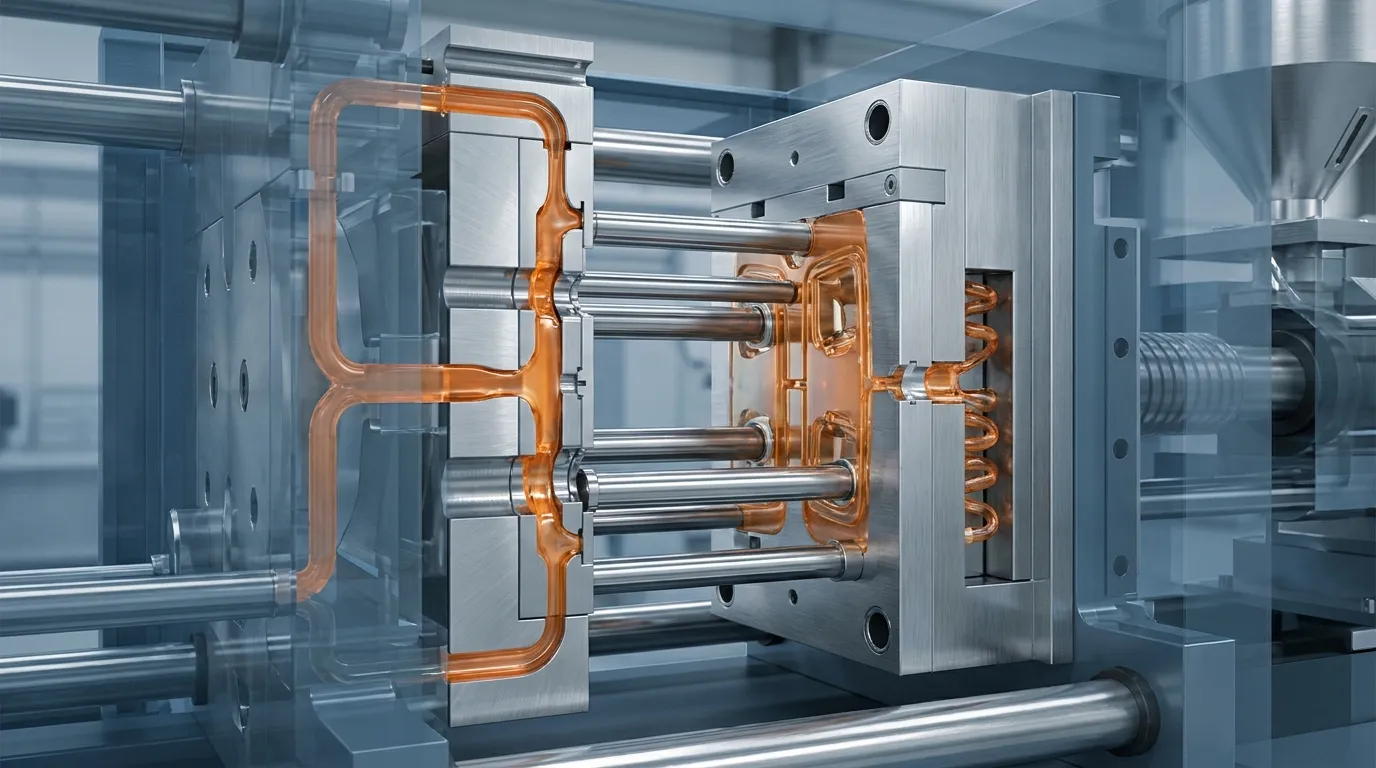
Core pins create internal geometry by occupying space inside the mold cavity while molten plastic flows around them. Tras el enfriamiento, the remaining void becomes the finished hole, channel, or internal feature in the molded part.
The molding cycle starts when the mold closes and molten resin enters the cavity under pressure. The core pin blocks plastic from filling a specific area. Resin flows around the pin surface instead, shaping the surrounding geometry during injection and packing. Medios electrónicos explains that this process is essential for creating internal molded features without secondary machining.
Durante la inyección y el empaquetado
Pressure inside the cavity can become extremely high, especially in thin-wall parts or glass-filled materials. If the pin is too thin or unsupported, it may deflect slightly during injection. That small movement can create oval holes, Deriva dimensional, or uneven wall thickness.
This problem appears often in connector housings and medical parts with micro-features. A medical housing mold using thin carbide pins may hold tight tolerances successfully, but only if the pin length and support geometry are balanced carefully.
Durante el enfriamiento y la eyección
Cooling also affects final hole quality. Uneven heat transfer around the pin can cause shrinkage differences in the molded plastic. Some molds add support sleeves or optimized cooling channels to stabilize temperatures around long pins.
Tras el enfriamiento, the mold opens and the part ejects. The core pin must release cleanly without dragging or sticking. If resin shrinks too tightly around the pin, ejection force rises and surface damage becomes more likely.
Which materials are used for core pins?
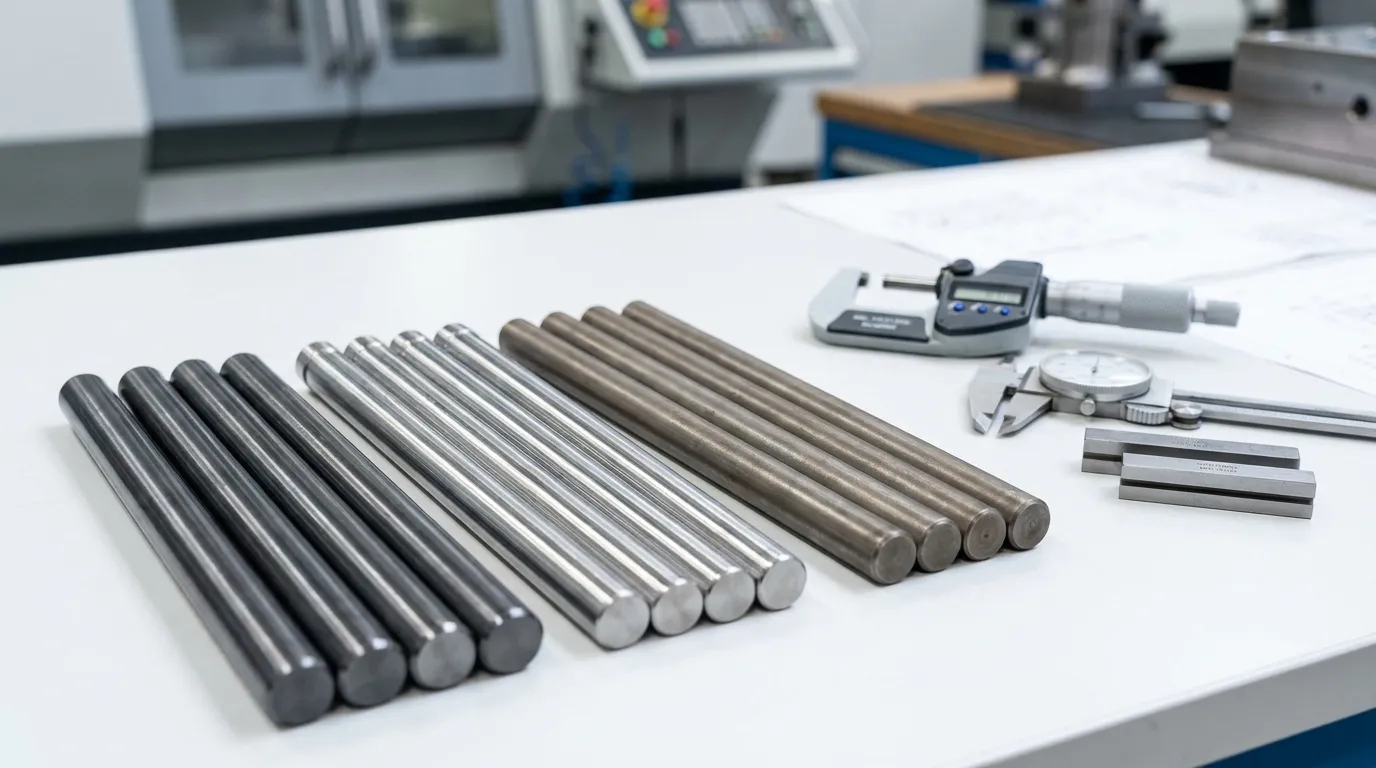
Core pin material selection depends on resin abrasiveness, Exposición a la corrosión, and tolerance requirements. Stainless steel works well for corrosive environments, while carbide performs better in high-wear applications such as glass-filled plastics.
Different molding conditions place different stresses on a core pin. Heat cycling, Presión de inyección, resin chemistry, and abrasive fillers all affect pin life. Choosing the wrong material can shorten maintenance intervals dramatically.
A standard tool steel pin may work perfectly for low-volume consumer parts. The same pin could wear rapidly in an automotive mold running glass-filled nylon 24 hours a day. Falcon CNC Swiss highlights carbide as a strong option for high-wear molding environments.
| Material | Mejor caso de uso | Principal ventaja | Limitación principal |
|---|---|---|---|
| Acero para herramientas | Molduras generales | Rentable | Menor resistencia al desgaste |
| Acero inoxidable | Resinas corrosivas | Resistencia a la corrosión | Menor resistencia al desgaste que el carburo |
| Carburo de tungsteno | Resinas rellenas de vidrio | Excelente resistencia al desgaste | Mayor coste |
Carbide is not always the best option. It performs well in abrasive applications, but stainless steel is often safer for corrosive resin systems. PVC and flame-retardant materials can attack standard steels over time, especially in humid production environments.
A high-volume bottle cap mold is one practical example. Switching from stainless to carbide pins may extend maintenance intervals significantly when abrasive additives increase wear rates. Aun así, carbide becomes harder to justify for low-volume molds with moderate tolerances.
For molds requiring specialized geometries, many manufacturers use Pines de molde personalizados designed specifically for the part shape and resin type.
What problems can poor core pin design cause?
Poor core pin design can cause dimensional drift, Flash, warped holes, Partes adherentes, and premature pin failure. Thin unsupported pins and incorrect material selection are common causes of molding quality problems.
Core pins directly affect molded part quality because they control internal geometry. Even minor pin movement during injection can create visible defects or tolerance issues. Cooling imbalance around the pin may also distort the surrounding plastic.
Una carcasa de electrónica de consumo es un ejemplo común. If a long unsupported pin sits near uneven cooling zones, the finished hole may become slightly oval after shrinkage. That small defect can create assembly problems later.
Guía de diseño de refrigeración UPMold shows how cooling imbalance contributes to warpage and dimensional inconsistency during molding.
Tabla de resolución de problemas de fallos de pines del núcleo
| Problema | Causa probable | Condición del pasador | Solución recomendada |
|---|---|---|---|
| Destello alrededor del agujero | Movimiento de pasador | Soporte suelto o desgastado | Mejora el ajuste de soporte |
| Agujeros ovalados | Desviación de los bolos | Clavo largo y delgado | Aumentar el diámetro o soporte |
| Atascado durante la eyección | Contracción excesiva | Desgaste superficial | Pulido o pasador de abrigo |
| Desgaste rápido | Resina abrasiva | Erosión del acero | Actualización a carburo |
| Marcas de quemadura cerca de la característica | Mala ventilación | Acumulación de calor | Mejorar la ventilación y la refrigeración |
Very thin pins may create complex geometry successfully, but unsupported long pins increase the risk of deflection during production. High precision tolerances become difficult to maintain once thermal movement and repeated pressure cycles enter the process.
Cooling matters just as much as machining accuracy. Some molds fail dimensional inspections because the thermal balance around the pin changes during long production runs. Better cooling layout often solves the issue faster than tighter machining tolerances.
If molded parts also rely on ejection around internal features, understanding Diseños de mangas eyector can help reduce sticking and part damage.
Core pins vs ejector pins: what is the difference?
Core pins shape internal features, while ejector pins push finished parts out of the mold after cooling. Core pins usually remain stationary during molding, while ejector pins move during the ejection stage.
These two mold components often get confused because both appear as cylindrical pins inside the tool. Their functions are completely different. Core pins create geometry. Ejector pins remove the finished part from the mold.
Opro-Tech explains that core pins participate directly in cavity shaping, while ejector systems activate only after cooling.
| Característica | Pines principales | Clavijas eyector |
|---|---|---|
| Función principal | Agujeros/características de forma | Pieza moldeada de empuje hacia fuera |
| Movimiento | Normalmente estacionaria | Movimientos durante la eyección |
| Posición en el ciclo | Inyección y refrigeración | Etapa de eyección |
| Principal problema de desgaste | Deflexión y abrasión | Deslizamiento repetido |
The distinction matters during mold design reviews. A buyer focused only on ejector placement may overlook critical support requirements for long core pins. That oversight can create expensive tooling corrections later.
For broader tooling comparisons, la Sistemas de eyección de moho section explains how ejection components interact with molded part release. Engineers comparing different component categories can also review the Guía de pasador eyector for additional tooling details.
What should engineers check before approving a core pin design?
Before approving a core pin layout, engineers should verify support length, Selección de materiales, cooling exposure, and expected resin wear conditions. Small design compromises often become production failures after high-volume cycling starts.
Long unsupported pins are one of the biggest warning signs. A small connector feature may look acceptable in CAD, but repeated injection pressure can bend the pin slightly during production. Support sleeves or geometry changes are sometimes safer than pushing tolerance limits too aggressively.
Matriz de selección de material de los pasadores principales
| Tipo de resina | Nivel de desgaste | Riesgo de corrosión | Material recomendado | Compensación |
|---|---|---|---|---|
| PP estándar | Bajo | Bajo | Acero para herramientas | Menor coste |
| Nailon relleno de vidrio | Alto | Bajo | Carburo | Mayor coste de herramientas |
| Resina ignífuga | Medio | Alto | Acero inoxidable | Desgaste más rápido que el carburo |
| Resina medicinal | Medio | Medio | Acero inoxidable | Buena resistencia a la corrosión |
Lista de verificación de aprobación
- Verifica el diámetro del pin en función de la longitud sin soporte
- Revisa la abrasividad de la resina y el contenido de relleno
- Comprueba la disposición de refrigeración cerca de los pines largos
- Confirma las expectativas de tolerancia con el volumen de producción
- Inspecciona las ventilaciones alrededor de las estructuras estrechas
- Revisar la accesibilidad de reemplazo para mantenimiento
High precision tolerances are meaningless if cooling balance is poor. Some molds achieve excellent machining accuracy initially, then drift during production because heat distribution changes around the core area.
Para ingenieros que necesitan una visión más amplia Visión completa del componente del molde, the pillar guide explains how core pins interact with cooling systems, Cavidades, Eyectores, and other tooling elements across the full mold structure.
Acertando en el siguiente paso
Core pins injection molding systems look simple at first, but they influence part quality, Vida útil de la herramienta, Frecuencia de mantenimiento, and production stability more than many buyers expect. The right pin material and support design can prevent flash, hole distortion, and early wear before production even starts.
If you're reviewing a new mold design, focus on resin type, unsupported pin length, Balance de refrigeración, and expected production volume first. Those factors usually matter more than chasing the tightest possible tolerance on paper. For more complex tooling decisions, reviewing the Guía de diseño de moldes de inyección can help connect core pin choices to the broader mold system.
Preguntas frecuentes
What is a core pin in injection molding?
A core pin is a precision mold component used to form holes, Tragaperras, and internal features inside molded plastic parts. It stays inside the cavity while molten resin flows around it during injection and cooling.
What is the difference between a core pin and an ejector pin?
Core pins create internal geometry inside molded parts, while ejector pins remove the finished part from the mold after cooling. Each component works during a different stage of the molding cycle.
What materials are core pins made from?
Core pins are commonly made from tool steel, Acero inoxidable, or tungsten carbide. The best material depends on wear conditions, Exposición a la corrosión, Abrasividad de la resina, y volumen de producción.
Can core pins cause molding defects?
Sí. Poorly designed or worn core pins can create flash, dimensional variation, sticking issues, and distorted holes. Long unsupported pins are especially vulnerable to movement during injection.
Why do core pins wear out?
Core pins wear out because of repeated heat cycles, resin abrasion, and injection pressure. Glass-filled plastics and corrosive resins usually increase wear rates faster than standard materials.
How accurate are injection mold core pins?
Precision core pins can hold extremely tight tolerances when they are properly supported and cooled. High-precision molds may achieve micron-level consistency depending on the material and production conditions.
Compartir:



Escrito por Sunshine
Al sol, Somos un fabricante y proveedor profesional de componentes de moldes de precisión, ofreciendo una amplia gama de productos para aplicaciones de estampado y moldes de inyección. Nuestro enfoque principal es el punzonamiento de troqueles, Pasadores y fundas eyector, y postes guía y casquillos. Con mecanizado CNC avanzado, Control de calidad estricto, y una fuerte capacidad de producción, Garantizamos la fiabilidad, Piezas de alta precisión, junto con componentes estándar en stock para un suministro global rápido y eficiente.
NOTICIAS
CONSIGUE EL SERVICIO
Con piezas de calidad para todos los presupuestos y personal amable formado para que tu visita sea informativa y sin complicaciones.
